
If you want one sentence: FDM printers with a large build volume handle wearable armor and oversized props, while MSLA resin printers handle fine detail and tight-fitting parts, and the best all-round buy for cosplay props in 2026 is the Anycubic Photon Mono M7 Max paired with a large-bed FDM machine for anything bigger than a mask.
That two-pronged answer matters because cosplay is the rare hobby where the same build can need two completely different machines. A chest plate is a large, hollow, lightweight, painted FDM part. The buckle, the belt greeble, the trim ring on a helmet visor, and the socket where a blaster half-connects to your forearm are resin work. Buy one printer and you compromise on both. Buy two and you have solved the problem properly.
We went through the current generation of consumer and large-format machines that actually print cosplay-scale geometry, read the owner review data on each, and ranked ten of them. The picks below cover resin detail work, enclosed multi-color FDM, large-format armor, and long-format props. Every printer here has a build volume that clears at least a full-size mask or a segmented armor plate, which rules out the small 150 mm cubes that dominate entry-level listings.
One thing worth saying up front: we are working from aggregated owner review data and published specifications, not from a lab bench. Where a machine has a documented reliability complaint, we say so instead of skipping it. The beginner’s guide to 3D printers covers the entry-level fundamentals if you have never printed before.
Top 3 Picks for Cosplay Props in 2026

Anycubic Photon Mono M7 Max
- 298 x 164 x 300 mm build volume
- 7K 13.6 inch LCD
- 1300 ml heated vat
- 60 mm/h with intelligent release

Bambu Lab P1S Combo
- Fully enclosed chamber
- Bundled AMS for 16 colors
- 500 mm/s with 20000 mm/s^2 acceleration

Bambu Lab A1 Combo with LED Kit
- AMS lite multi-color unit
- Full-auto bed and Z-offset calibration
- LED lamp kit for lit props
The Photon Mono M7 Max takes the top slot because it is the only machine in this roundup that combines a genuinely large resin build volume, a 1300 ml vat, and the deepest owner review base we found at over 2000 ratings. The P1S Combo earns the value badge because an enclosed chamber plus a 16-color AMS changes what a costume can look like after painting, and it does it without a second machine on your desk.
The A1 Combo is the cheapest honest route into multi-color printing, and the bundled LED lamp kit is a genuinely cosplay-shaped accessory. It is open-frame, which is the trade-off you accept for the lower entry point.
Best 3D Printers for Cosplay Props Compared in 2026
| Product | Specifications | Action |
|---|---|---|
| Anycubic Photon Mono M7 Max |
|
Check Latest Price |
| Bambu Lab P1S Combo |
|
Check Latest Price |
| Bambu Lab A1 Combo with LED Kit |
|
Check Latest Price |
 QIDI Max4 Combo |
|
Check Latest Price |
 Creality K2 Plus Combo |
|
Check Latest Price |
 Anycubic Kobra S1 Max Combo |
|
Check Latest Price |
 IdeaFormer IR3 V2 Belt Printer |
|
Check Latest Price |
 Anycubic Photon P1 Max |
|
Check Latest Price |
 Elegoo Saturn 4 Ultra 16K |
|
Check Latest Price |
 Phrozen Sonic Mega 8K S |
|
Check Latest Price |
Five of these are resin machines and five are FDM. That split is not arbitrary. Resin wins on surface finish, dimensional accuracy, and small-part detail; FDM wins on size, material choice, cost per gram, and the ability to print a hollow wearable part that will not snap when you drop it. Read the next section before you decide which half of the split your build needs.
1. Anycubic Photon Mono M7 Max – Best Detail and Size for Full-Size Masks
ANYCUBIC Photon Mono M7 MAX Resin 3D Printer, 13.6’’ 7K Large Resin Printer
MSLA resin
298 x 164 x 300 mm
7K 13.6 inch LCD
1300 ml heated vat
52.8 lb
Pros
- 298 x 164 x 300 mm volume fits full-size masks
- LighTurbo 3.0 engine with 90 percent light uniformity
- Dynamic vat temperature control
- Resin auto-fill and one-key recycling
- Most owner reviews in the group at over 2000 ratings
Cons
- Resin still needs washing curing and careful handling
- 10 percent of ratings sit in the one-star bucket
- 52.8 pounds of machine on your desk
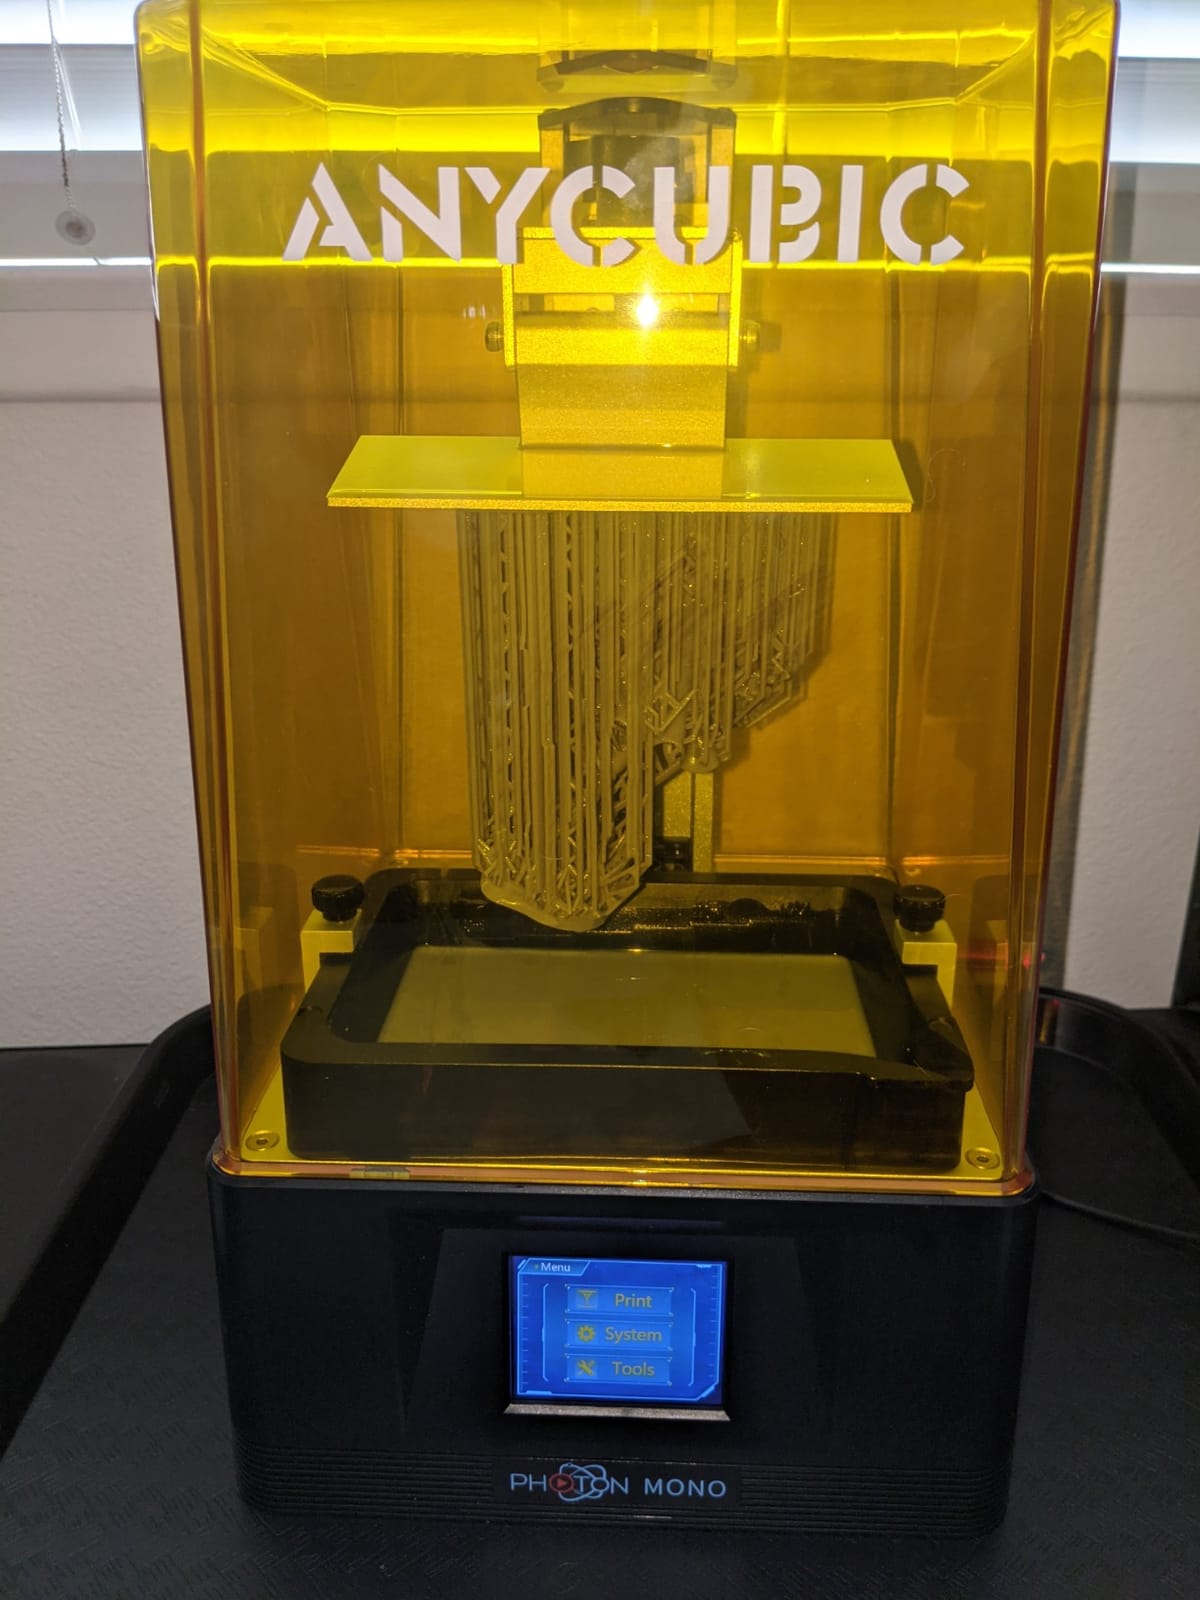
The M7 Max solves the problem that kills most resin buys for cosplay, which is that the build volume is too small for the part you actually want. At 298 x 164 x 300 mm it takes a full-size human mask in one pour on its side, and the 1300 ml vat means a chest ornament or a pair of pauldrons can go in the same run. That is a very different proposition from a 7 inch resin machine that needs a mask split into four pieces and glued back together with visible seams.
Detail is where this machine earns its rating. The LighTurbo 3.0 COB light source sits behind a Fresnel lens with factory calibration to within three degrees, and owners report light uniformity above 90 percent across the panel. On a finished prop that translates to clean edges on a visor rim and a legible emblem on a shoulder plate, without hours of scraping layer lines.
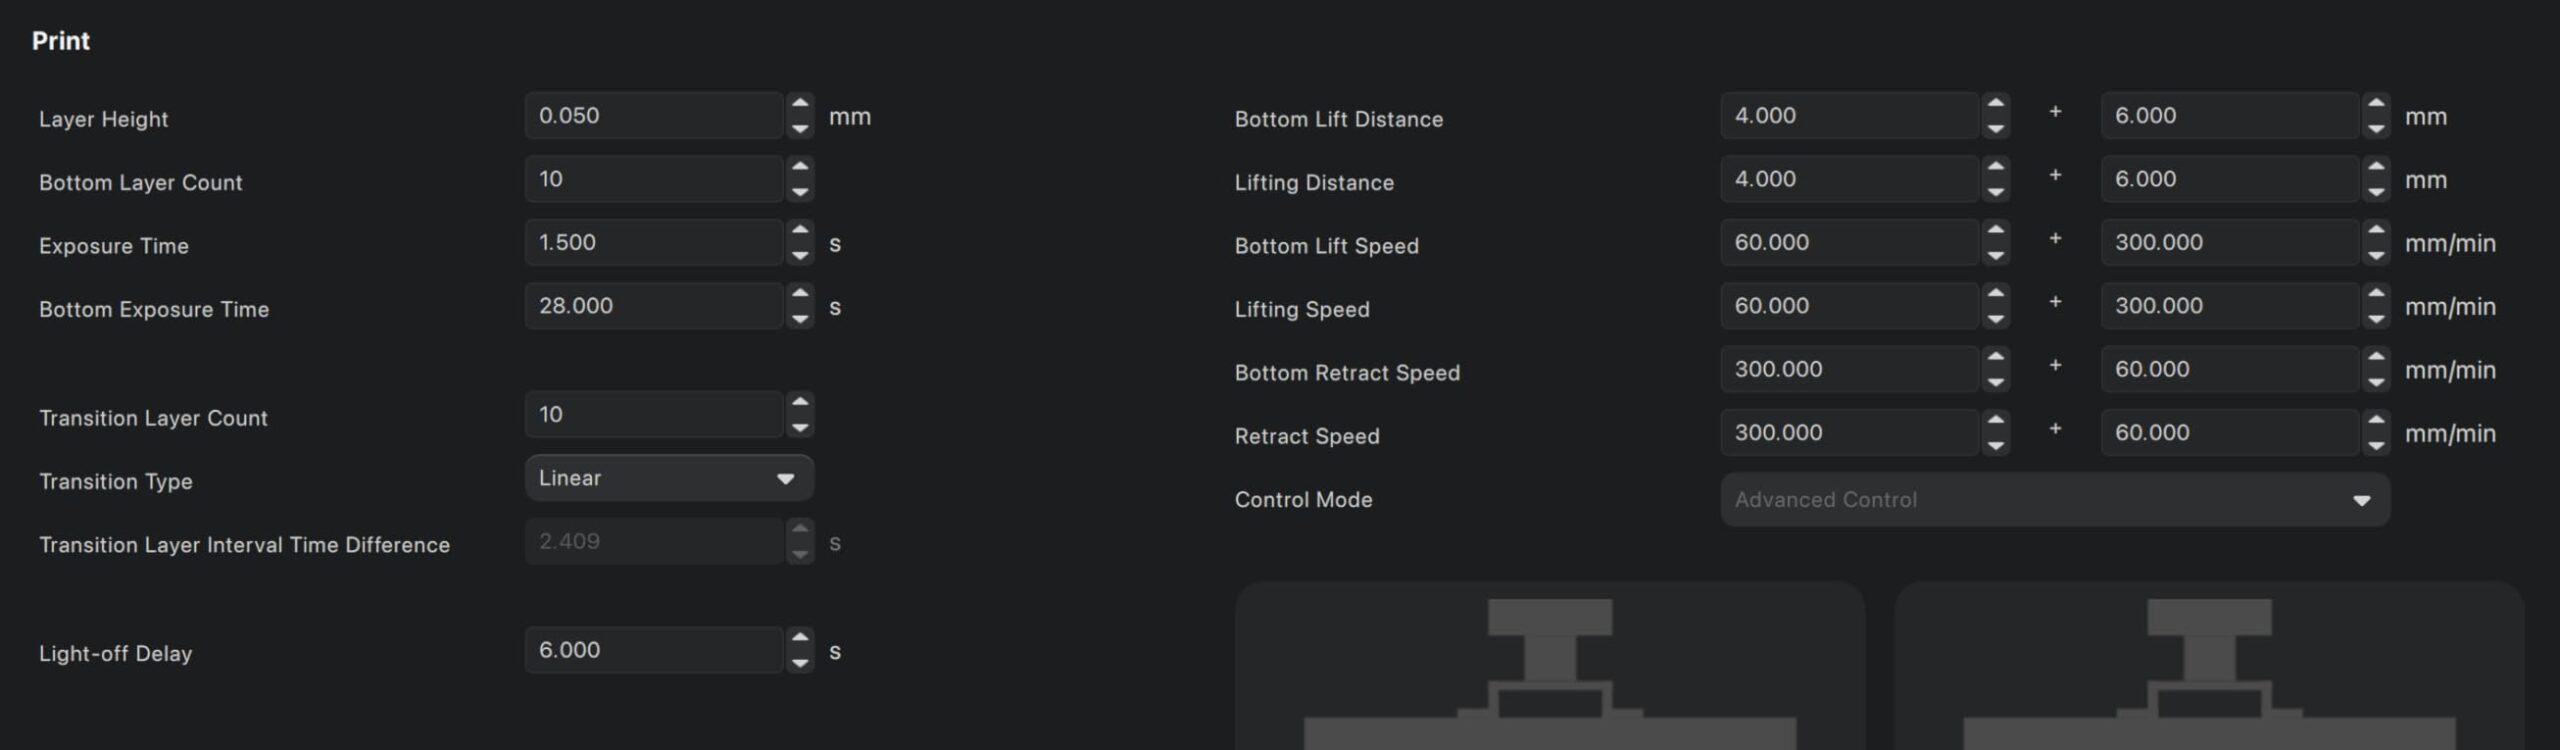
The intelligent release 2.0 system is a claimed 200 percent speed increase over the previous M7 Max generation, and reviewers with hundreds of hours on it describe layer separation as rare rather than routine. The dynamic temperature-controlled vat is the part that matters most for cosplay specifically: large thin resin shells cure unevenly when the vat is cold, and this one holds temperature through the job.
Resin auto-fill and one-key recycling of whatever is left in the vat are the two features that will save you the most money over a costume project. Buying a bottle, pouring it in, and recovering the remainder beats guessing at fill lines and throwing away a partial bottle every time.
What the M7 Max does well for cosplay
It is the single best value for mask-scale resin work in this list, because the resolution and the volume are both there. A mask printed in tough resin comes out of the wash looking like something you would spend real hours cleaning up, and the 13.6 inch panel gives you the XY pixel density to hold a thin crest or an undercut jaw line that a smaller screen smears.
It also pairs naturally with a foam or FDM build. Print the structural shell and mounting brackets in a large FDM machine, print the face plate, ear pieces, and trim in resin here, and bolt them together. That hybrid approach is what experienced builders on r/cosplayprops describe as the normal way to handle large bulk sections.
Where the M7 Max is the wrong choice
Skip it if resin handling is a hard no. You are committing to nitrile gloves, a wash station, IPA, a UV curing station, and a ventilated room, and a printed resin prop is not a toy you can hand to a child without curing it properly first.
It is also the wrong tool for a piece that has to flex or take a hard knock. Resin is rigid and brittle in thin sections, so a gauntlet or a shoulder piece that will be bumped all convention weekend belongs in FDM tough filament instead. The 52.8 pound weight and 20 x 20 x 31 inch footprint also mean it needs a permanent shelf, not a laptop desk.
2. Bambu Lab P1S Combo – Best Value Enclosed Multi-Color FDM
Bambu Lab P1S Combo, P1S 3D Printer and AMS, Multi-Color 3D Printing
Enclosed FDM
16-color AMS included
500 mm/s
PLA to ASA and PC
47.5 lb
Pros
- Enclosed chamber handles ABS and ASA
- AMS bundled for up to 16 colors
- Printing within one to two hours for first-time users
- Auto bed leveling on every print
- Large model library in Bambu Studio
Cons
- On-screen display is low resolution and awkward
- Default SD card files will not run with the AMS
- No filament spools included
- A small number of defective hot end reports
The P1S Combo is the machine we recommend to someone whose costume is mostly large painted armor with a handful of accent colors. The enclosure is the reason. A heated chamber that holds temperature is what separates a clean ABS or ASA print from a delaminated one, and enclosed FDM is the difference between a chest plate that survives a con floor and one that delaminates in the first layer.
The bundled AMS is the second reason. Multi-material printing through an AMS removes the single most tedious part of finishing a prop, which is hand-painting stripes, trim, and secondary colors onto a helmet or a boot. Owners consistently describe the AMS as making multi-color work straightforward rather than fiddly, and the unit carries four spools, with expansion to sixteen through additional units.
Set-up is the quiet headline. The manufacturer quotes roughly fifteen minutes and owners report first prints within one to two hours of unboxing, which matters enormously when you are learning to slice on the same weekend you are trying to get a prop finished. Auto bed leveling runs on every print, so a mesh that drifts after you move the machine is not a mid-project crisis.
Speed is not a gimmick here. 500 mm/s with 20000 mm/s squared acceleration is well into the range where a 20 hour chest plate print becomes a 12 hour one, and the acceleration figure matters more than the top speed on large armor because most of a big print is travel, outer wall, and infill at moderate feed rates.
Why cosplay builders pick this one
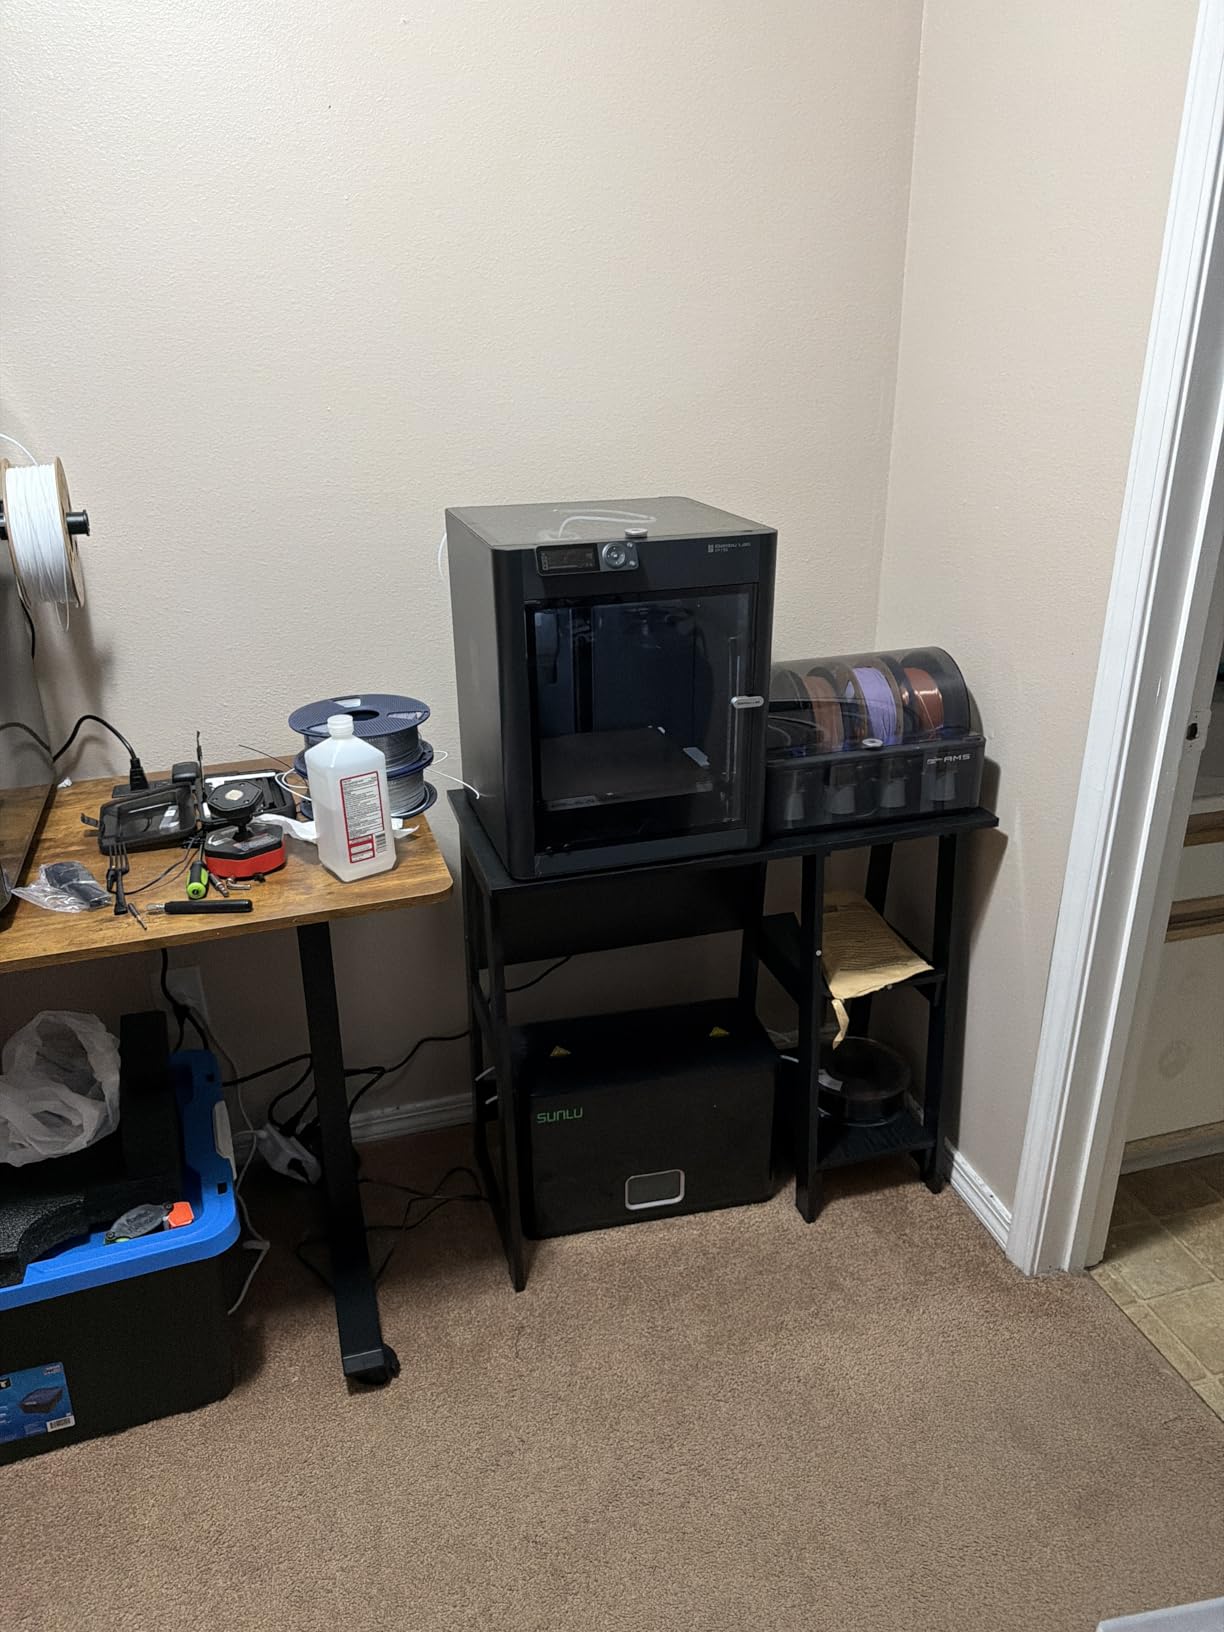
A Halo builder on the 405th forum reported ordering a P1S with no regrets and getting ODST shoulder pieces that came out essentially perfect, which is exactly the kind of multi-part accuracy report that matters when you are bolting left and right pieces together and need them to mirror correctly. Multi-color accuracy is a real purchase factor here and almost no competing guide covers it properly.
It is also the easiest machine in this list to grow with. PLA and PETG cover 90 percent of cosplay work, TPU handles soft goods and straps, and ABS and ASA cover vehicle interiors and heat-exposed display pieces. The P1S is not recommended for carbon or glass fiber reinforced polymer, which is worth knowing before you plan an armor build around CF- nylon.
What to know before you buy
The built-in screen is the most common complaint. It is low resolution and awkward to navigate, and in practice most owners stop using it and slice from a laptop or a phone once the machine is set up. Budget ten minutes with the app on first use instead of fighting the panel.
Two smaller things catch people out. The files that come on the bundled SD card do not work with the AMS, so any multi-color job has to be sent from the app rather than the card. And no filament spools are included, so budget for PLA, PETG, and an ASA spool in your first order. A small number of buyers also report defective hot ends and repeated error messages, so keep the packaging and test the hot end early rather than the week of the convention.
3. Bambu Lab A1 Combo with LED Kit – Best Budget Route Into Multi-Color Printing
Bambu Lab A1 Combo + LED Lamp Kit, Multi-Color 3D Printing (with AMS lite)
Open-frame FDM
AMS lite 4-spool
10000 mm/s^2
28.5 lb
LED kit included
Pros
- Lowest entry point to multi-color printing
- LED lamp kit lights printed props in place
- Full-auto Z-offset and bed leveling
- Quick swap nozzle for easy maintenance
- Lightest machine here at 28.5 pounds
Cons
- Open frame rules out ABS and ASA work
- AMS lite holds only four spools
- 14 percent of ratings are one-star
The A1 Combo is the machine to buy if your budget is the deciding factor and you mostly need PLA and PETG. It ships with the AMS lite, which is a four-spool multi-material unit, so multi-color accents on a costume are available without a separate purchase. That alone puts it a tier above every single-extruder machine on the market at this level.
The LED lamp kit is an odd inclusion that turns out to make sense for cosplay. Illuminated props, glowing visor slits, and lit edge detailing on a chest piece are all achievable in multi-material PLA, and the bundled lamp lets you check how the light reads on the finished piece instead of guessing. Very few printer bundles are designed around a display use case at all.
Calibration is fully automatic for Z-offset and bed leveling, and there is a 1-Clip quick swap nozzle that makes a hot end change a desk job rather than a teardown. Active motor noise canceling keeps it quiet enough to run in a shared apartment, which matters when your con deadline is Friday and the printer lives in the room you sleep in.
Acceleration of 10000 mm/s squared is lower than the machines above it, so the top speed is not what this one is for. What it is for is learning the workflow on a machine that will not punish beginner mistakes, and then knowing exactly which upgrades you want later.
Where this machine fits a cosplay build
Gauntlets, bracers, buckles, boot props, trim, and costume accessories are all comfortably inside this build envelope. Anything with a large flat painted surface is where you will see layer lines most, so plan on filler primer and sanding before you commit to a hero piece. Our resin printer guide for miniatures covers the alternative if the finish is the priority.
It is also a good second machine to run alongside a resin printer in a shared space, because it is small, light, and quiet enough to live on a shelf rather than a workbench.
Where the open frame bites
The single most important limitation is that the frame is open. There is no chamber, so there is no way to hold ABS or ASA at the temperature those materials need, and warping on anything larger than a hand-sized part becomes a real risk. If your build includes a car interior, a fire prop, or anything that will sit in a hot car on the way to the venue, this is the wrong machine.
Four spools is also a hard ceiling on the AMS lite. Complex multi-color characters with skin tone, hair, costume, and trim can exhaust that quickly, and swapping filament mid-print is not seamless. And at 14 percent one-star, this is the highest critical share among the Bambu machines listed, so give it a full test print before committing a whole costume to it.
4. QIDI Max4 Combo – Best for Full-Size Armor in One Piece
QIDI Max4 Combo 3D Printer, 390×390×340mm Build Volume, 65℃ Heated Chamber
Enclosed FDM
390 x 390 x 340 mm
65 C chamber
800 mm/s
120 lb
Pros
- Largest build volume in the roundup
- Prints full-size helmets in one piece
- 65 C chamber runs ABS-CF PC and PPS-CF
- No manual leveling needed out of the box
- Full-surface silicone heated bed
Cons
- 120 pounds needs a dedicated sturdy table
- QIDI BOX magazine tangles and will not auto-switch
- Thin documentation for a machine this complex
Every sizing question in this hobby comes back to one number, and on the QIDI Max4 that number is 390 x 390 x 340 mm. That is 55 percent more volume than the previous generation, and it is the difference between printing a full-size helmet in a single piece and printing it in quarters. If your build includes a chest plate, a back plate, and a helmet that all need to look continuous, that extra space removes an entire category of seam problems.
The 65 C active heated chamber is the second headline. That is hot enough for ABS-CF, PC, and PPS-CF engineering materials, and for cosplay that translates to ABS and ASA prints that do not lift at the corners of a large flat plate. A full-surface silicone heated bed gives even temperature across 390 mm, which is what keeps a big first layer stuck down through a 30 hour job.
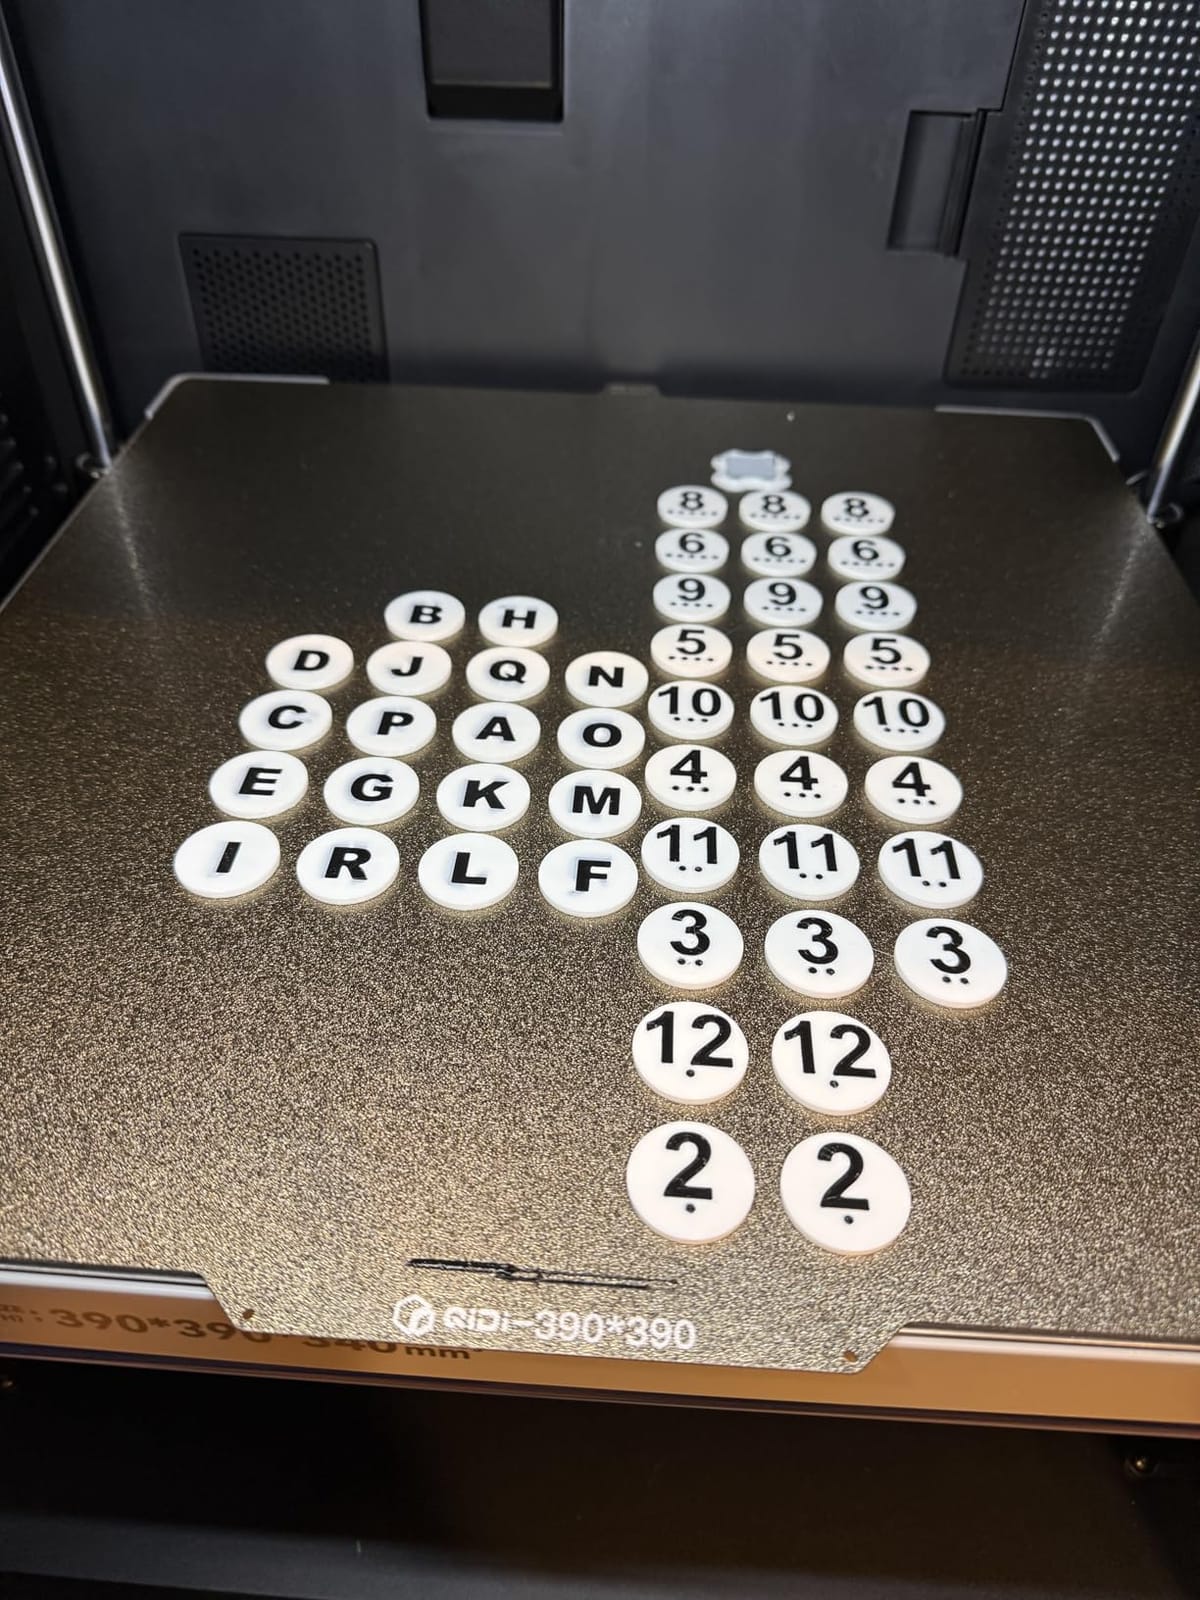
Owner reviews describe flat, consistent bed adhesion after a single calibration, closed-loop motors on X and Y, and a 2 mm lead screw with an anti-backlash nut on Z. At 800 mm/s with 30000 mm/s squared acceleration, a large armor print is dominated by wall and infill time rather than travel, and one reviewer reports printing thousands of meters of filament without a clog, which is the failure mode that actually ends large jobs.
The built-in AI camera detects failures and pauses the print, and the hot end is a 40 mm cubed per second high-flow unit with a hardened steel nozzle. Those are the features that make a machine you might run for six hours a night, every night for a month before a convention, a realistic proposition.
Who this is genuinely for
Someone with a deadline and a large, mostly flat, mostly painted build who has already printed before. This is not a first printer. The owner reports in the review data come from people running heavy cosplay and prop workloads near-continuously, and multiple detailed reviews describe strong support response and parts shipped with tracking, which matters when a machine breaks mid-project.
If your armor is full-scale and you want it in one piece, this is the answer. If you are building gauntlets and props at a more modest size, the volume is wasted capability and the P1S Combo does the job for considerably less.
What gives us pause
It weighs 120 pounds. That is not a desk printer, it is a floor-standing piece of equipment that needs a table rated for it, and moving it between rooms is a two-person job. The Polar Cooler is sold separately and not included, so chamber management for the hottest materials is an extra purchase.
Multi-color through the QIDI BOX is the weak spot. Owners report the magazine can tangle and does not auto-switch spools, and integration with OrcaSlicer is unreliable, so plan on single-color prints here and treat multi-color as a bonus. The instruction documentation is also sparse for a machine this complex, and with only 30 owner ratings the long-term data is thinner than the specification sheet suggests.
5. Creality K2 Plus Combo – Best Multi-Color Throughput
Creality K2 Plus Combo 3D Printer, Multi Color Printing with New CFS 600mm/s High-Speed Full Auto-Leveling Dual Al Camera Next-Gen Direct Drive Extruder Large Build Volume 13.78×13.78×13.78inch
Enclosed FDM
350 mm cube
CFS to 16 colors
600 mm/s
60 C chamber
70.4 lb
Pros
- 350 mm cube handles large props without splitting
- CFS units scale to 16-color printing
- Very high speed for a large-format machine
- Chamber heating and hardened nozzle for ASA and PPA
- Dual AI cameras and 18 sensors
Cons
- 17 percent of ratings sit in the one-star bucket
- 70.4 pounds and a large footprint
- Low installed base means less community support data
When multi-color is the whole point of the build, the K2 Plus Combo is the machine to look at. The CFS system handles four colors per unit, and up to four CFS units can be linked for 16-color printing. For a character costume with skin tone, hair, undersuit, trim, and two accent colors, that is the difference between a printed prop and a painted one.
The 350 x 350 x 350 mm build volume is a true cube, which is unusual and genuinely useful. A cube means a helmet fits in any orientation, and a chunky prop like a shoulder-mounted cannon or a thick boot can be laid down rather than tilted to maximize the diagonal.
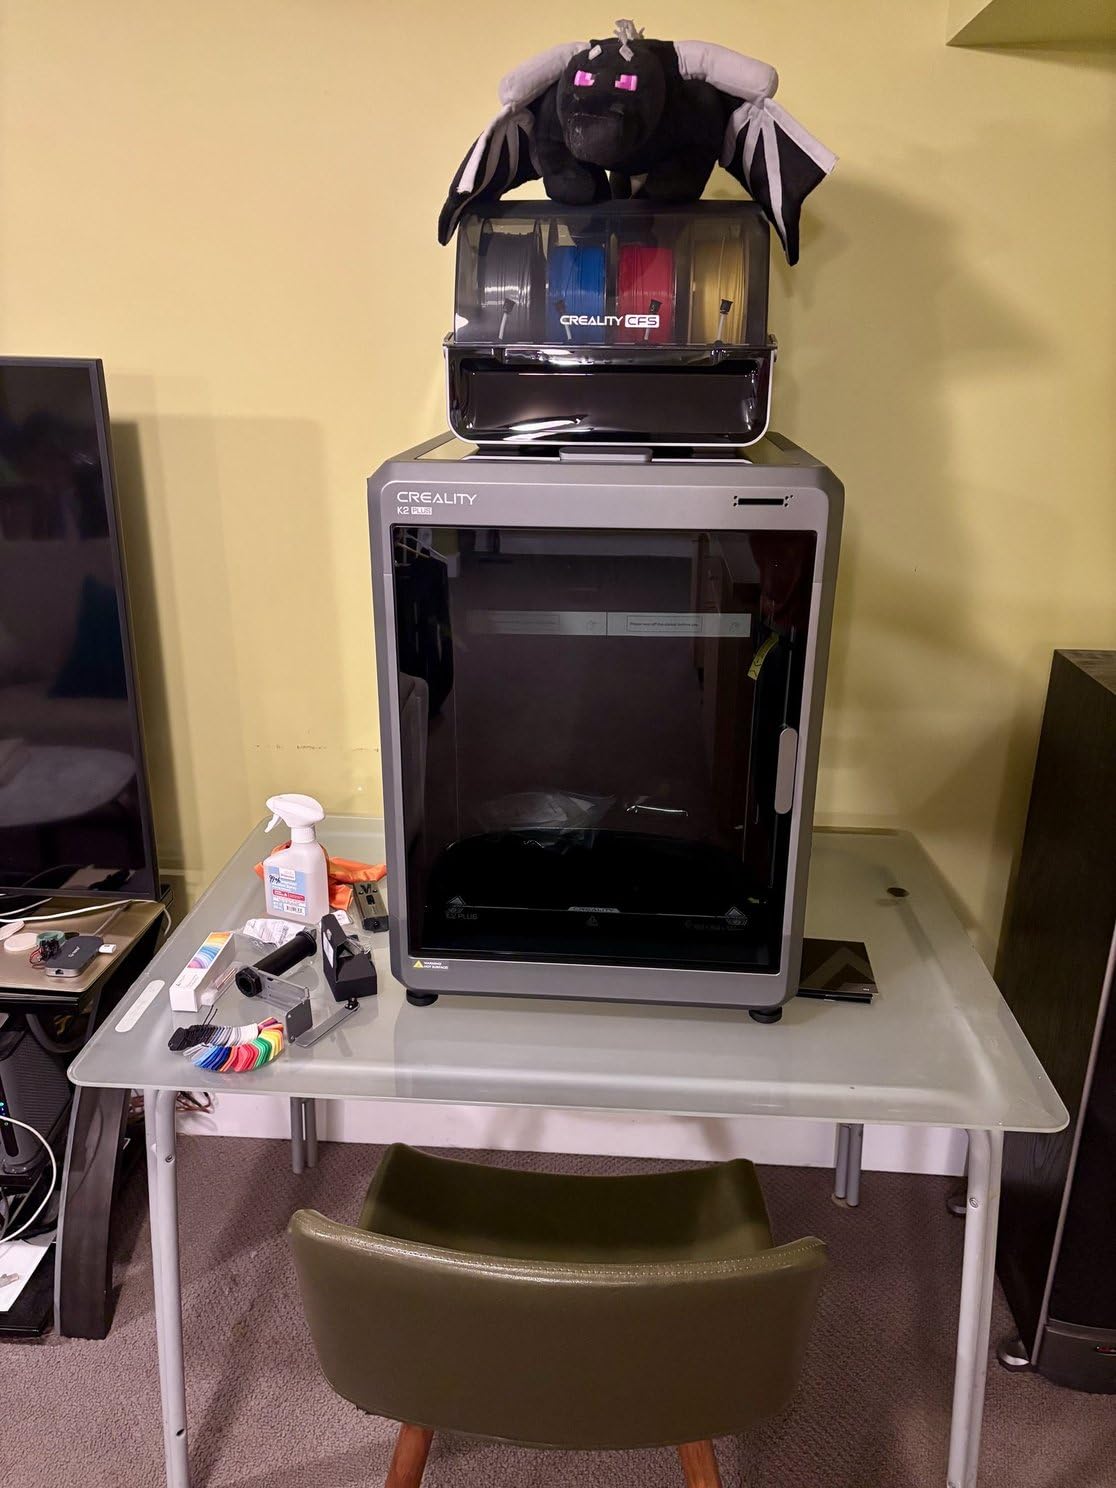
Speed and thermal performance are the other strengths. 600 mm/s with FOC step-servo motors and 30000 mm/s squared acceleration on a 40 mm cubed per second flow hot end is a lot of throughput for a machine this size, and chamber heating to 60 C with a nozzle rated to 350 C opens up ASA and PPA alongside standard PLA and PETG.
The monitoring hardware is unusually thorough: dual AI cameras on the chamber side and the toolhead, plus 18 smart sensors. On a long unattended print that is the difference between finding a failed layer at hour six and finding a ruined plate at hour thirty. The dual independently motorized Z-axis with four linear rods and auto bed tilt correction also means a large flat armor plate stays dimensionally true as the build grows.
Where this machine earns its place
Multi-color at scale, and large prints at speed. The matrix die-cast aluminum alloy frame is rigid enough to hold precision at those speeds, which is what lets it print a 30 hour armor job without the corners drifting. Dual AI cameras also let you check on a print remotely, which is the single most useful feature when a deadline is real.
If your costume is a printed figure or a small prop at figure scale rather than a wearable, this is overkill. Our large-format printer guide covers the sizing question in more detail.
What to watch out for
The rating distribution is the biggest flag. At 4 stars overall with 895 ratings, the split is 66 percent five-star and 17 percent one-star, and that one-star block is the largest in this roundup among the well-reviewed machines. On a machine this new, a meaningful share of critical reviews usually means early hardware revisions, so treat the first week as a shakedown period and keep packaging.
It also weighs 70.4 pounds and measures 16.1 x 15.4 x 18.7 inches, so it is a floor or sturdy-shelf machine rather than a desktop one. And with a smaller installed base than the Bambu machines, the community knowledge and slicer profile library you can borrow is thinner.
6. Anycubic Kobra S1 Max Combo – Best High-Speed Large-Format All-Rounder
Anycubic Kobra S1 Max Combo 3D Printer, Large Build Size 350x350x350 mm³
Enclosed CoreXY
350 mm cube
ACE 2 Pro 4-color
600 mm/s
65 C chamber
Pros
- 350 mm cube prints a helmet without splitting
- Enclosed all-metal CoreXY frame stays rigid at speed
- 65 C chamber prints ABS and ASA without splitting
- ACE 2 Pro includes filament drying
- LeviQ 3.0 49-point auto-leveling
Cons
- Slicer is locked to Anycubic software
- AI detection unreliable for some owners
- Frequent errors on long multi-color jobs
- Rare filament feeder defects
The Kobra S1 Max is the same 350 mm cube as the Creality K2 Plus with a different philosophy around the multi-material unit, and for some builds the bundled drying is the deciding factor. The ACE 2 Pro includes filament drying, and on a multi-color job that means four spools that have each picked up moisture sitting in a heated box rather than exposed.
Moisture is the quiet killer of cosplay FDM. A spool that has been open for two weeks produces popping, stringing, and rough surfaces on exactly the large flat panels you were trying to make look good, and owners running a printer as a production machine will have open spools almost all the time.
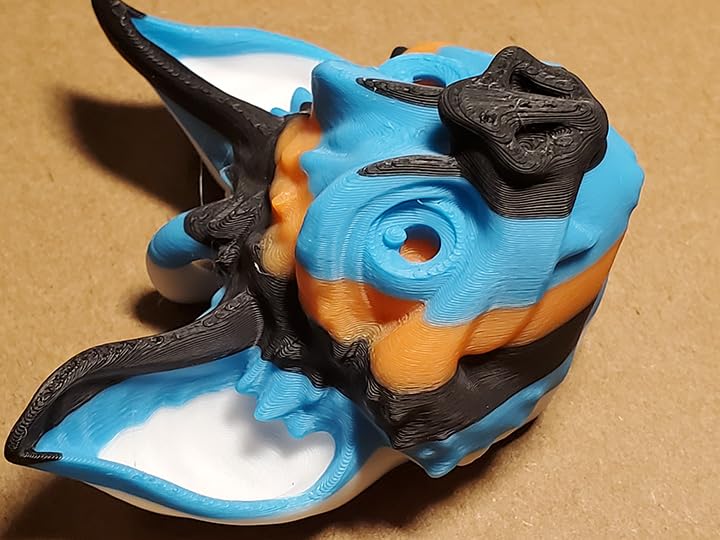
The mechanical platform is a fully enclosed CoreXY structure with an all-metal frame. CoreXY means the mass of the gantry does not move on a single axis during acceleration, and that is why this class of machine can hold 600 mm/s with 20000 mm/s squared acceleration on a large print without ringing artifacts on the outside wall.
LeviQ 3.0 does a 49-point auto-leveling pass with real-time flow dynamics calibration, and owners report clean first layers on large plates. The benchy reference print completes in roughly 15 minutes, which is a useful sanity check when you set the machine up rather than starting with a 20 hour chest plate.
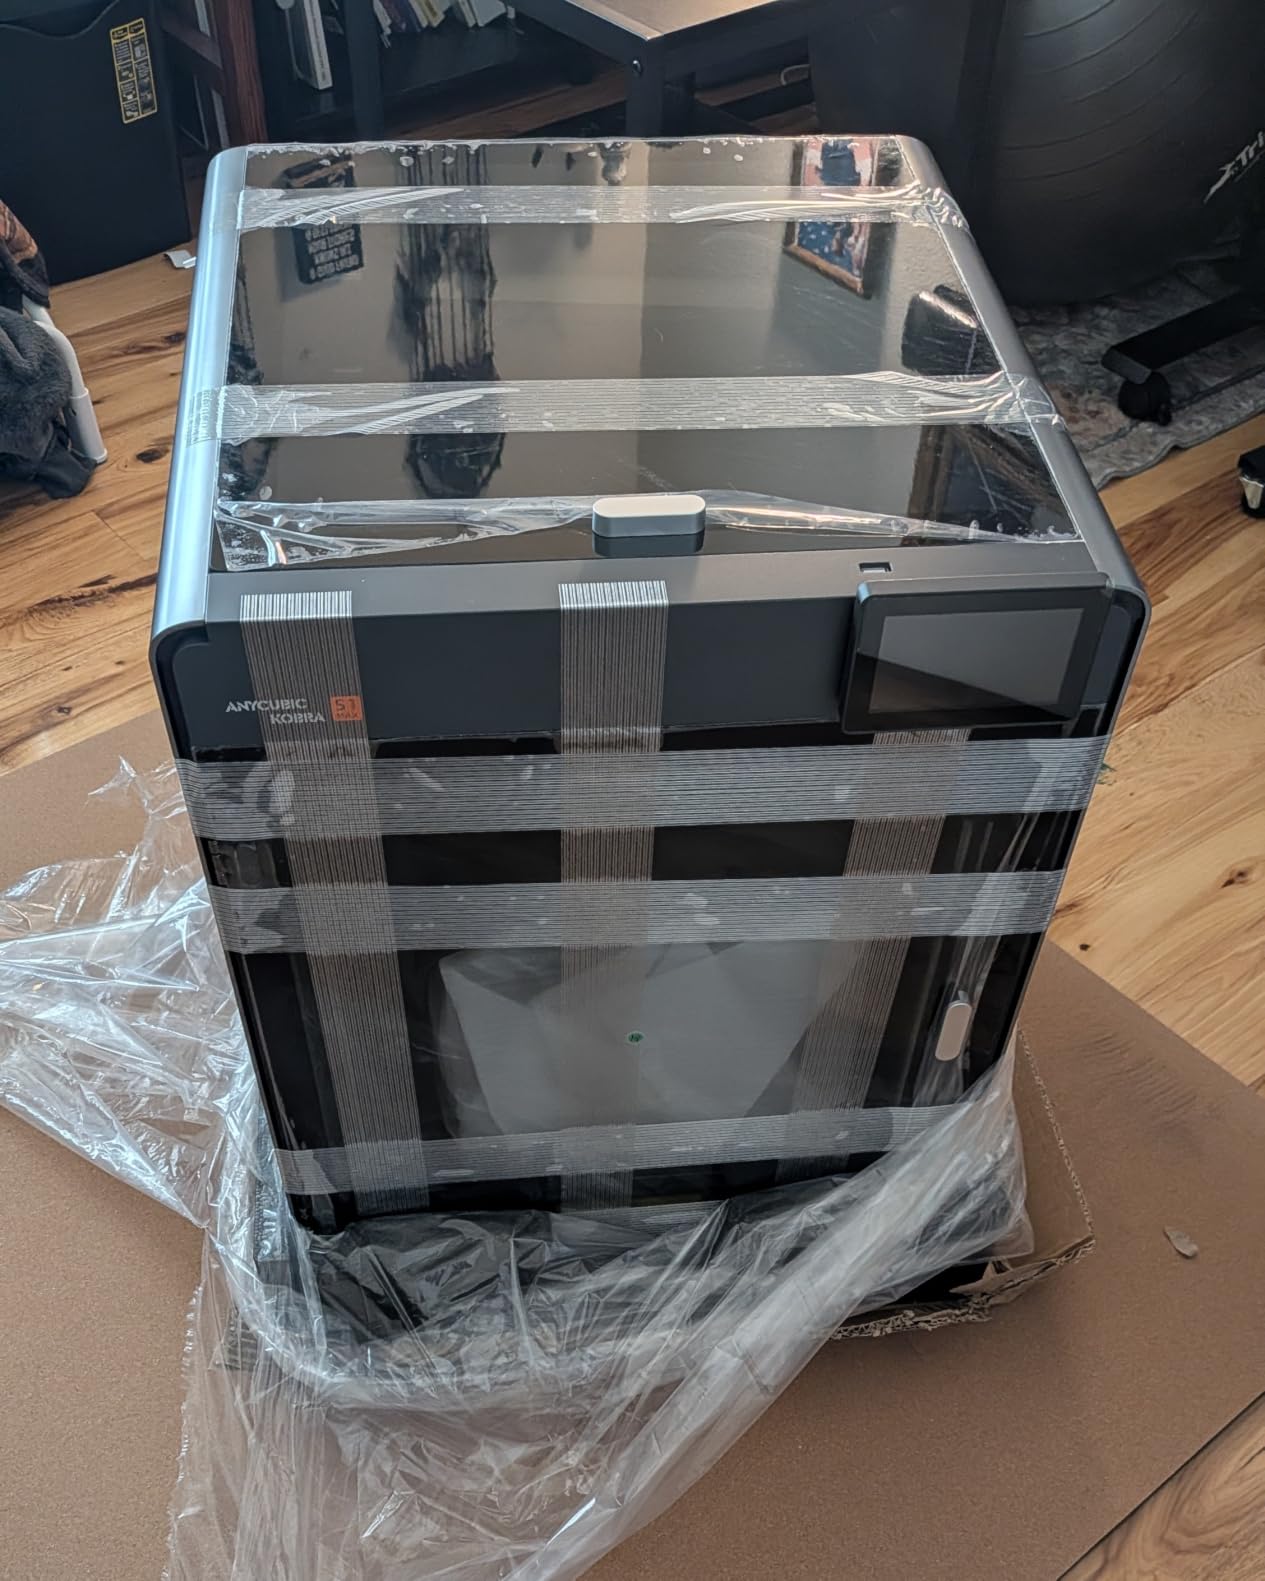
Why it suits a deadline build
The 65 C chamber and 350 C hot end combination means ABS and ASA print without layer splitting, which is the single most common way large cosplay FDM prints fail. Combined with a 350 mm cube, this machine handles a helmet, a chest plate, and a pair of pauldrons over a run of days without you slicing anything into sections.
Multi-color expands to 16 colors with four ACE boxes, and the large responsive touchscreen is a genuine step up from the low-resolution panels on some competitors. If your workflow is set-and-forget with a four-color budget, this configuration is well matched.
The compromise here is the software
The slicer is locked to Anycubic software. That is a real limitation: the community profile libraries and OrcaSlicer or PrusaSlicer workarounds that make other machines flexible are not available, and if you have already tuned profiles for a different machine you will be starting over.
Owners also report occasional spurious filament sensor errors, which are fixable by disabling detection, and AI detection that has been unreliable for some. Several buyers report frequent errors on long, complex multi-color jobs specifically, so for a marathon multi-color costume build, test a full color-change run before you depend on it. At 20 ratings the data here is early, and the 77.8 pound weight means a dedicated spot.
7. IdeaFormer IR3 V2 – Best for Long Props That Exceed Build Height
Official IdeaFormer-3D IR3 V2 Conveyor Belt 3D Printer, Infinite Z Axis Continuous Printing Belt Printer Large Format 250×250×∞mm for Cosplay, Prototyping & Production Auto Leveling 400mm/s Speed
Belt FDM
250 x 250 mm infinite Z
400 mm/s
Klipper firmware
44 lb
Pros
- Infinite Z prints a full-length blade in one piece
- Unattended queue-based serial production
- PEI belt parts pop off cleanly once cooled
- 45 degree layers print hollow parts without support
- Standard Klipper and Fluidd for easy customization
Cons
- Steep learning curve
- 45 degree gantry clashes with models designed for standard printers
- Belt adhesion shifts over time
- Belt and sensor failures reported in the first weeks
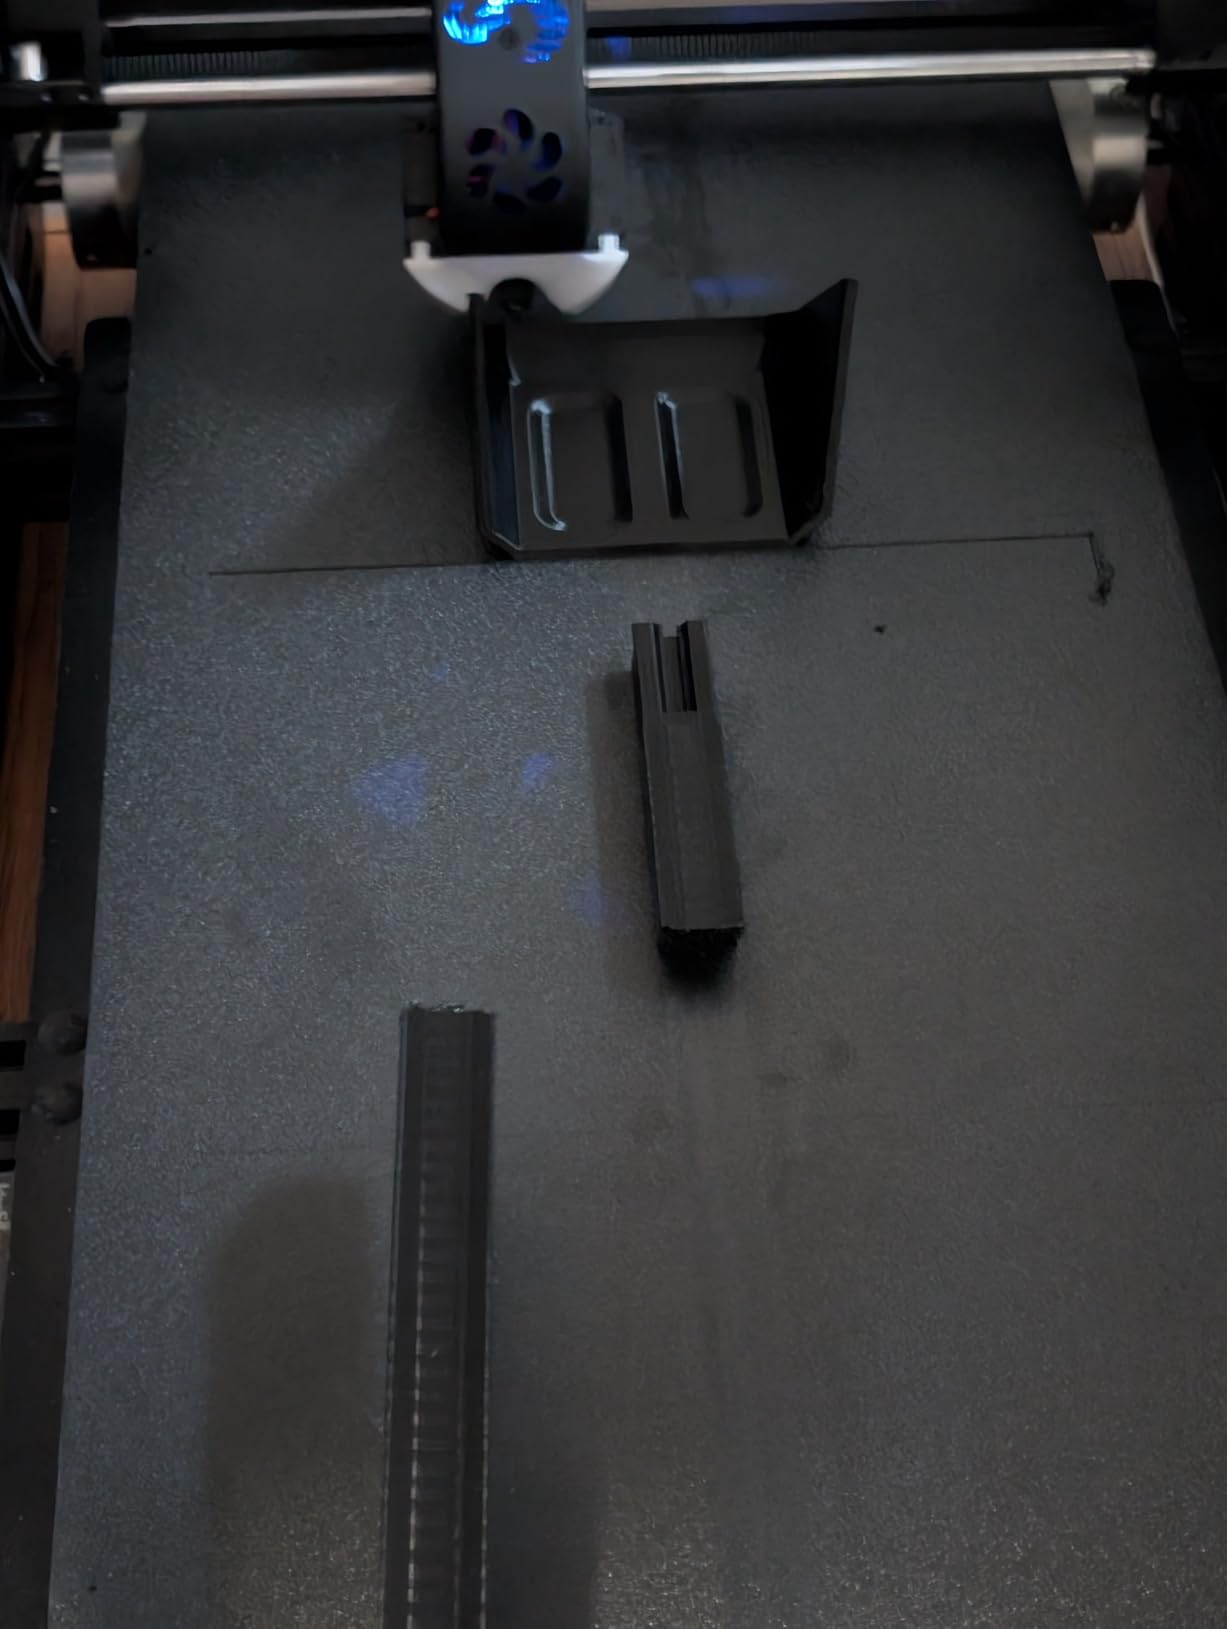
Almost every oversized prop problem in cosplay is a height problem, not a width problem. A seven foot sword, a spear, a scythe, a staff, a bow, a banner pole: these are long thin objects that fit comfortably on a 250 mm bed and simply do not fit in a 300 or 400 mm build height. The IR3 V2 solves that with a 45 degree conveyor belt instead of a Z axis, so the build volume in Z is genuinely infinite.
That is a narrow, weird, and extremely effective answer to a narrow, weird problem. If you are making one long prop, this machine prints it in a single piece with no seam, no alignment jig, and no splice. If you are making a chest plate, use something else.
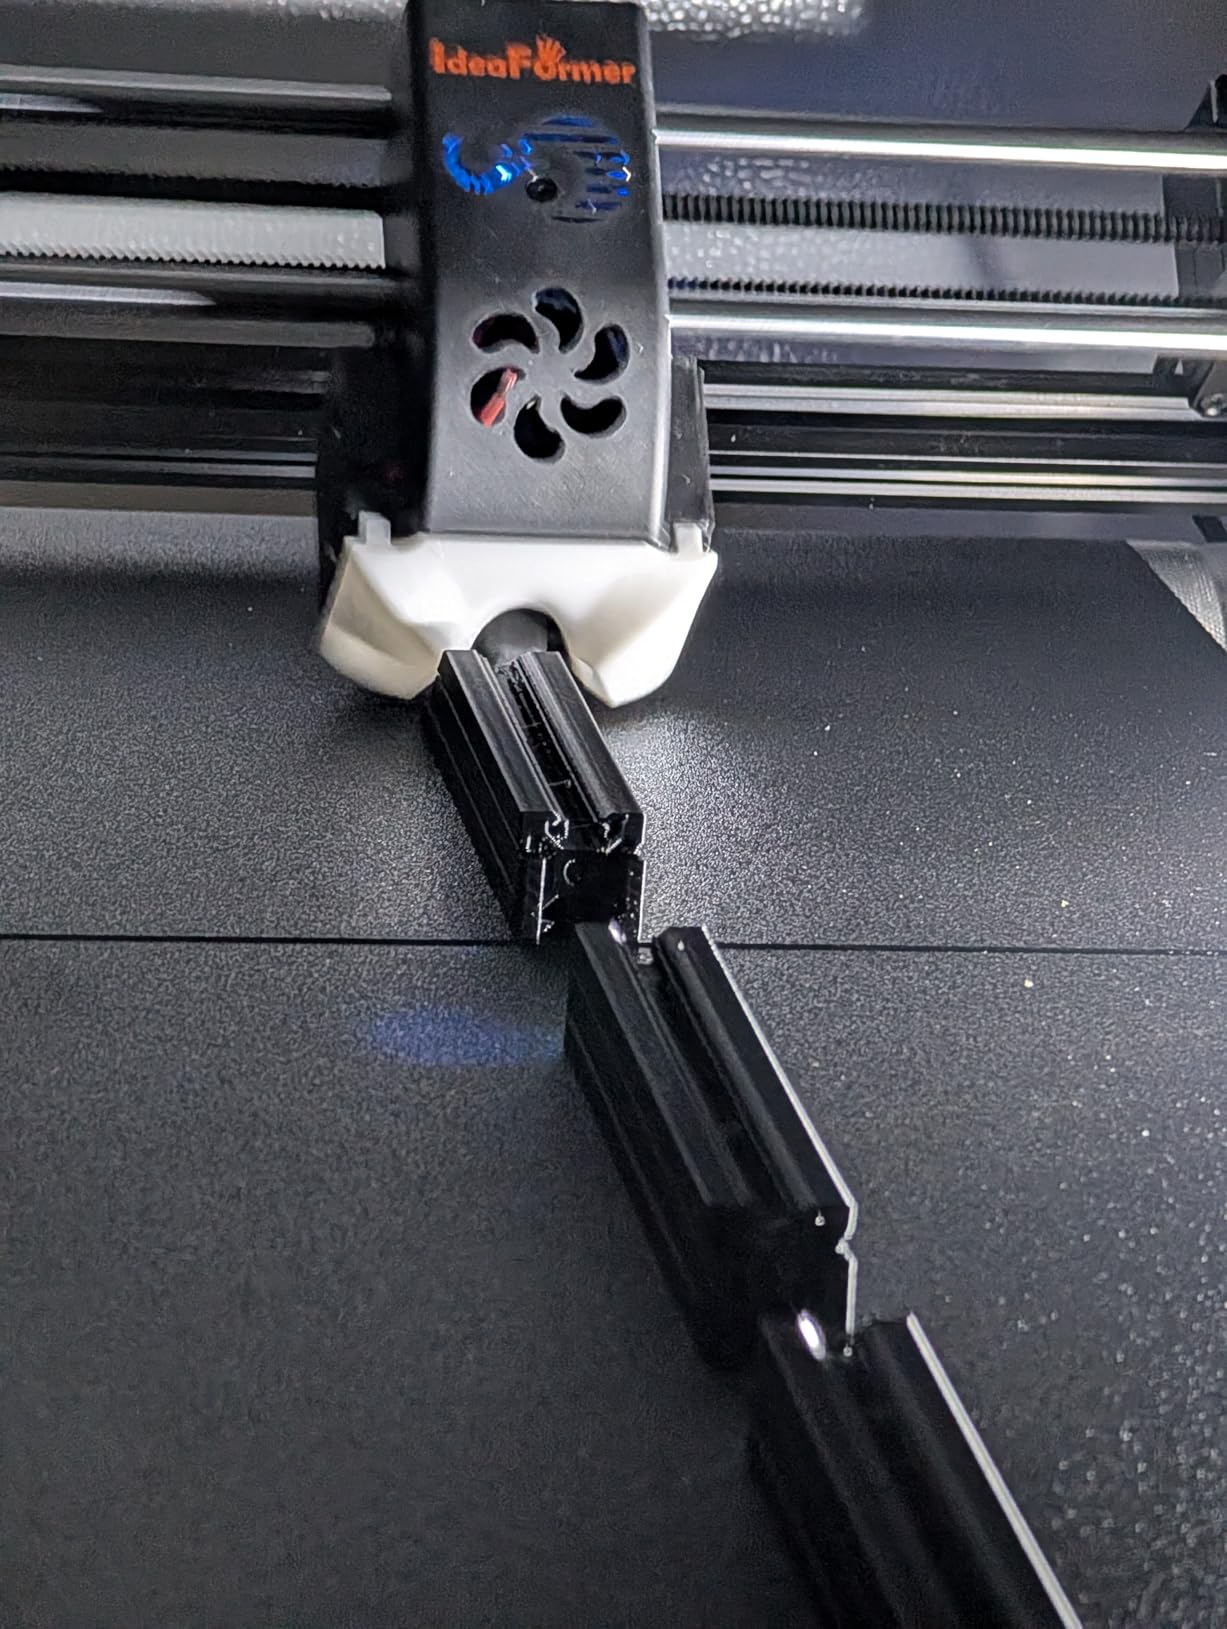
The 45 degree print angle is the second unexpected advantage. Because layers are laid diagonally, a hollow part prints with its interior open and needs no internal support, which on a long prop is the difference between a clean interior you cannot reach and an interior full of support material you have to cut out. The PEI coated metal belt also gives strong adhesion and releases cleanly once the part has cooled.
Production behavior is what owners praise most. The queue-based serial workflow runs unattended with very rare failures, and 400 mm/s with an integrated roller gearbox keeps a long job moving. Klipper firmware with a Fluidd web interface means you can monitor from a phone on the same network, which is exactly what you want for a print that runs for two days.
What it is genuinely brilliant at
Blade and shaft geometry, and the class of prop that experienced builders talk about constantly. A prop that has to collapse to fit into a standard suitcase for transport, as one builder described in a large-prop thread on r/cosplayprops, is really a segmentation problem, and a printer with infinite Z removes the segmentation problem for long objects entirely.
The belt accepts PLA, PETG, ABS, TPU, ASA, and PP, and TPU on a conveyor belt is a nice combination if you want a flexible grip or a costume-safe edge. One-click auto calibration with a Y-offset strain sensor handles the main drift, and customer support is reported as quick with replacement parts.
Why most people should not buy this
The learning curve is the first barrier. This is not a beginner machine, and the documentation is a real weak point, with some owners reporting sparse instructions. If you have never printed before, the P1S Combo or the A1 Combo will teach you the same fundamentals with far less friction.
More seriously, the 45 degree gantry creates overhang problems with models designed for a standard printer, so you may need to reorient or redesign parts. Belt adhesion shifts over time and needs recalibration after moving, and owners report belt damage, nozzle clogging, and filament sensor failures within weeks of purchase, with some arriving with damaged belts or missing parts. It is also noisier than a typical machine, comparable to an enclosed unit.
8. Anycubic Photon P1 Max – Best for Batch Resin Work
ANYCUBIC Photon P1 Max, Large Resin 3D Printer with Smart Tank Heating
MSLA resin
18.3 L build volume
12K 14 inch screen
1.9 L heated vat
59 lb
Pros
- 18.3 L volume takes oversized models or dozens of parts
- Plus or minus 0.01 mm repeatability for snap fits
- 12K screen reduces jagged edges on edges and faces
- 1.9 L heated vat handles viscous resin
- AI monitoring for plate level and layer separation
Cons
- Resin requires washing curing and safety handling
- 59 pounds and a large footprint
- Early release with a small owner base
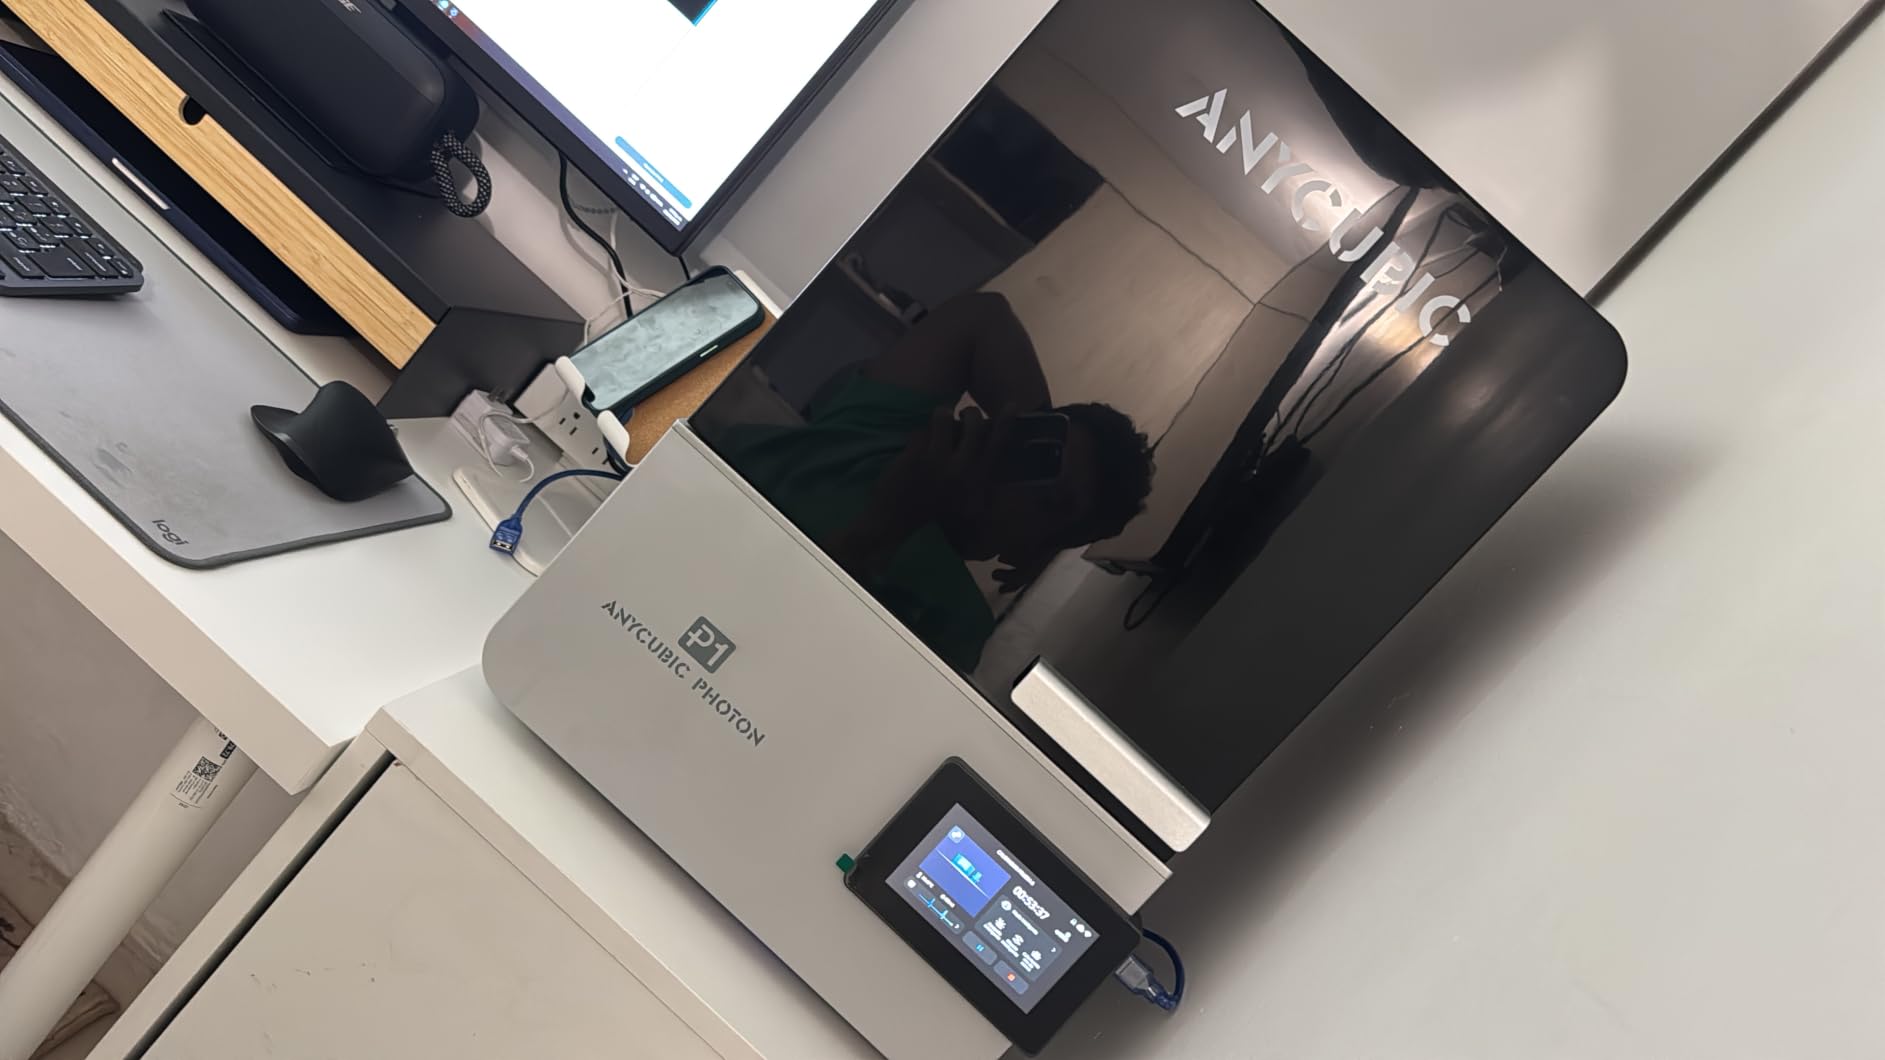
The Photon P1 Max is the resin machine to buy if resin is your primary medium and you are producing a full costume rather than a single detail piece. The 18.3 L build volume at 11.24 x 8.43 x 11.81 inches is large enough to batch a whole set of matching pieces in one pour, which is how resin actually makes economic sense on a costume project.
Repeatable accuracy of plus or minus 0.01 mm is the specification that matters for cosplay specifically. Snap fits, threaded sockets, and mating parts that have to assemble with the same piece printed two weeks earlier all live or die on repeatability, not on peak resolution. If your prop has a moving part or a press-fit connection, this is the number to shop on.
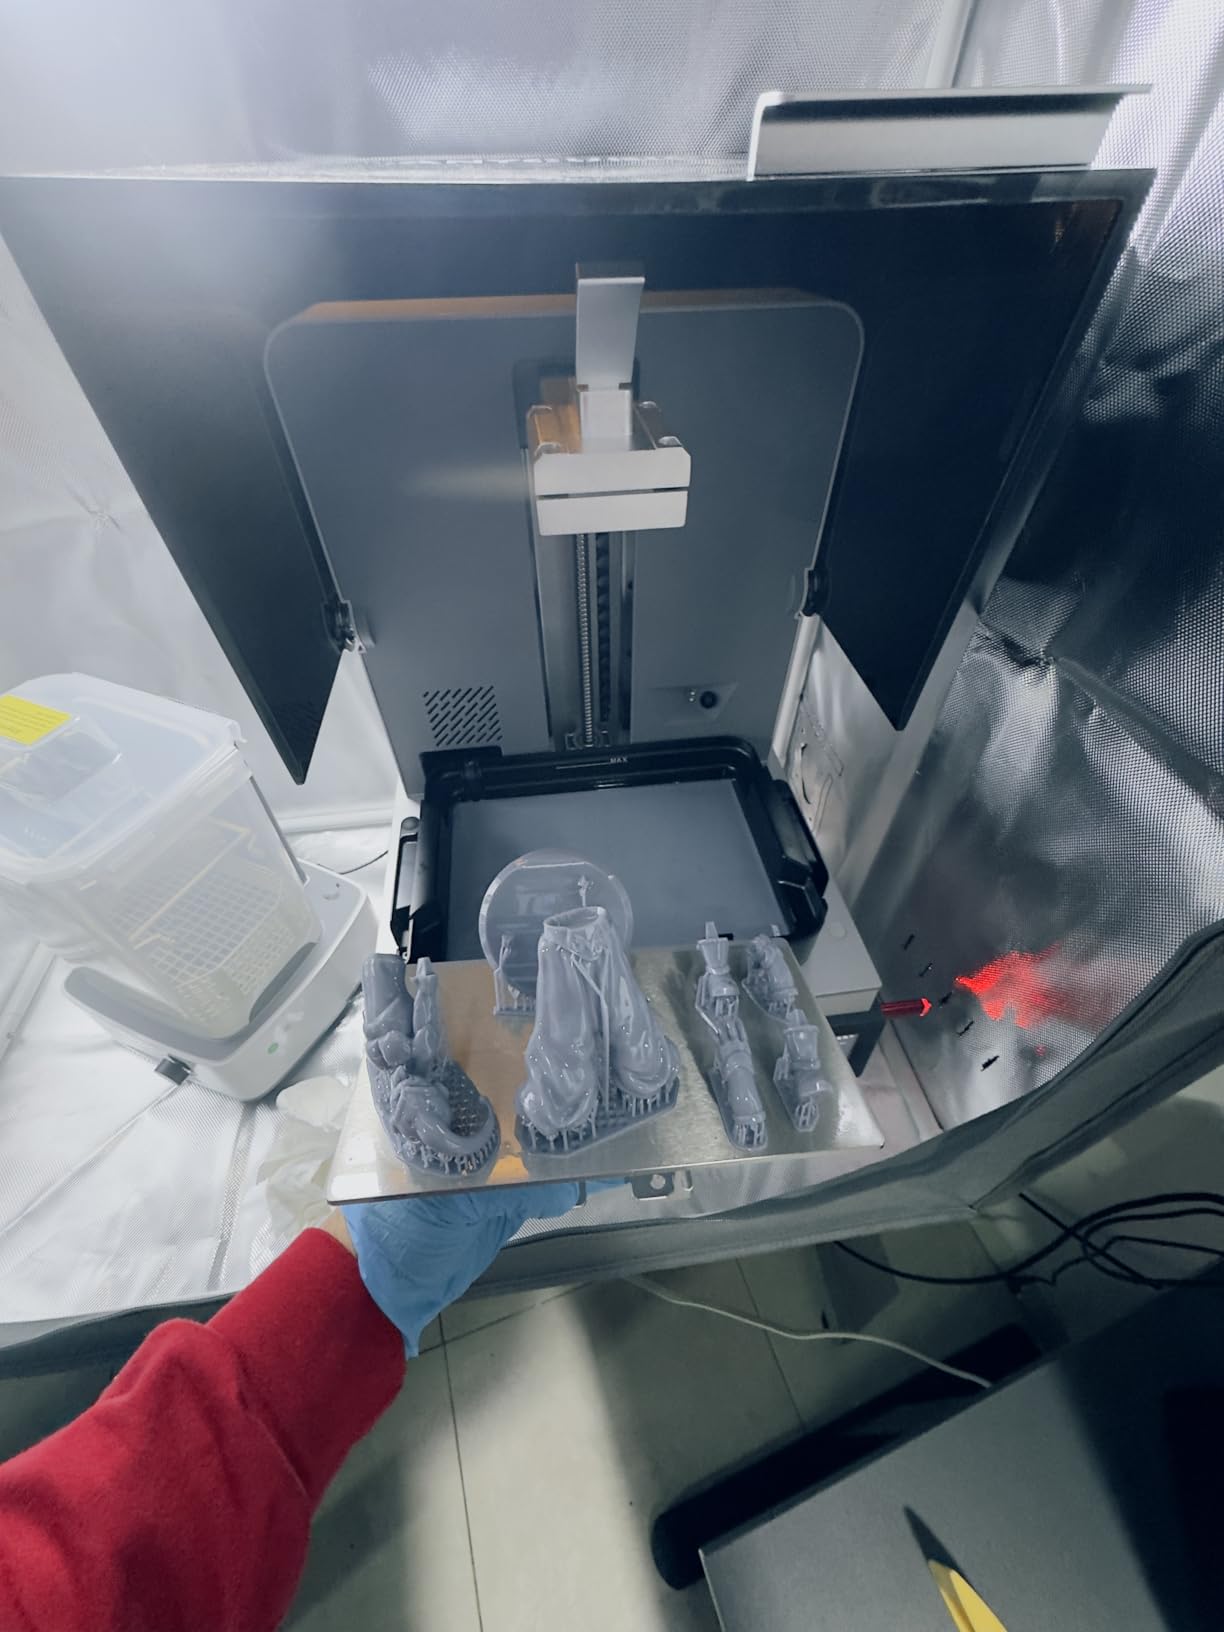
The 14 inch 12K screen with the LighTurbo 3.0 light engine is what handles the finish quality, reducing jagged edges and visible layer lines on curved surfaces. That is a helmet cheek, a pauldron curve, and a boot dome, which is where resin visibly beats FDM and where you will notice it most after painting.
Auto-Leveling 3.0 calibrates before every print and checks four corners in real time with live force readings, and the heated 1.9 L vat holds resin up to 35 C. Viscous resins used for tough and durable prop printing thicken in a cold room, and a heated vat is the difference between a successful large pour and a failed one on a cold convention weekend.
Where it earns the money back
Batch production. Print all the buckles, all the trim, all the matching caps and connectors in a single run and the cost per part collapses. The AI monitoring for build plate detection, resin level, bottom-layer separation, and vat residue is genuinely aimed at print-farm and engineering-team workflows, and it is the feature set most likely to catch a failure before it wastes a full vat.
It is also the best of these resin machines for large hollow pieces, which is where you hollow a shell, cut drain holes, and save most of the resin. Large hollow prints are exactly the resin technique that makes a big prop affordable, and the volume here supports it.
What to keep in mind
Resin is resin. This machine still requires washing, curing, ventilation, and nitrile gloves, and nothing in the specification sheet changes that, which is the honest reason resin deters first-time buyers. It weighs 59 pounds and measures 29.53 x 21 x 20.1 inches, so it needs a permanent location with ventilation.
It is also a recent release with a small owner base, so long-term reliability data is thin compared to the more established resin machines here. If you want proven longevity over cutting-edge batch capacity, the Mono M7 Max has the review depth to back it.
9. Elegoo Saturn 4 Ultra 16K – Best for Fine Resin Detail
ELEGOO Saturn 4 Ultra 16K Resin 3D Printer
MSLA resin
16K monochrome LCD
150 mm/h tilt release
30 C heated vat
35.5 lb
Pros
- 16K panel captures fine textures and smooth surfaces
- Heated vat at 30 C improves layer adhesion
- Automatic leveling with no manual adjustment
- Tilt release speeds up model peeling
- AI camera and chamber light for time-lapse
Cons
- Resin needs washing curing and safety handling
- 13 percent of ratings are one-star
- Smallest resin build volume of the group
The Saturn 4 Ultra 16K is the pick when the finished surface is the priority. A 16K monochrome LCD puts more pixels over a smaller area than any other resin machine here, and on a cosplay prop that means readable texture on a sculpted surface, a clean crisp edge on a blade, and fine detail on a small emblem or connector that a lower-resolution panel turns into mush.
For figure-scale cosplay accessories, kitbash accessories, and the small detail parts that sit on top of a large FDM build, that difference is the whole reason to own a resin printer at all. It is also why our resin guide for miniatures leans on panel resolution so heavily.
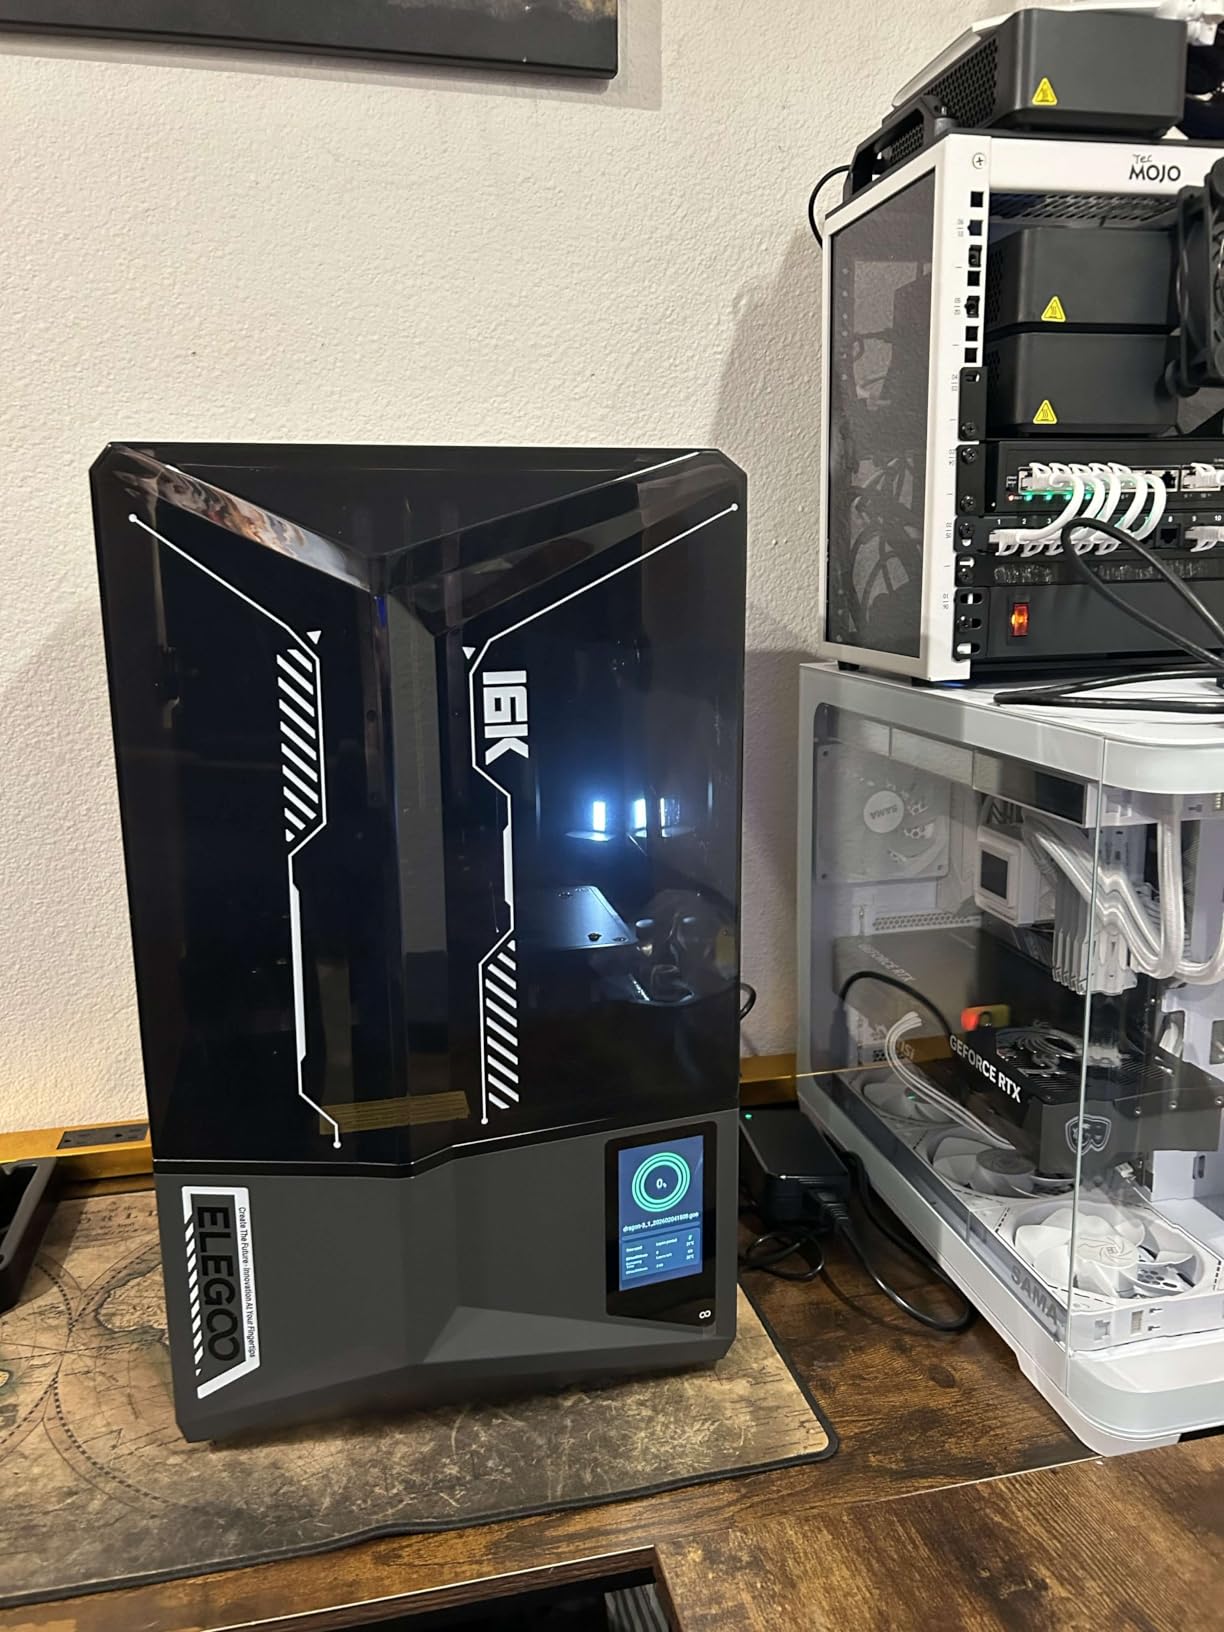
The smart tank heating holds the resin at 30 C. That sounds like a small number until you have watched a large thin shell fail to bond between layers because the vat was at 18 C, which is a common evening-room temperature. Warmer resin flows and adheres better, and it also cuts down on the bubble problem that pits a surface you then have to sand and fill.
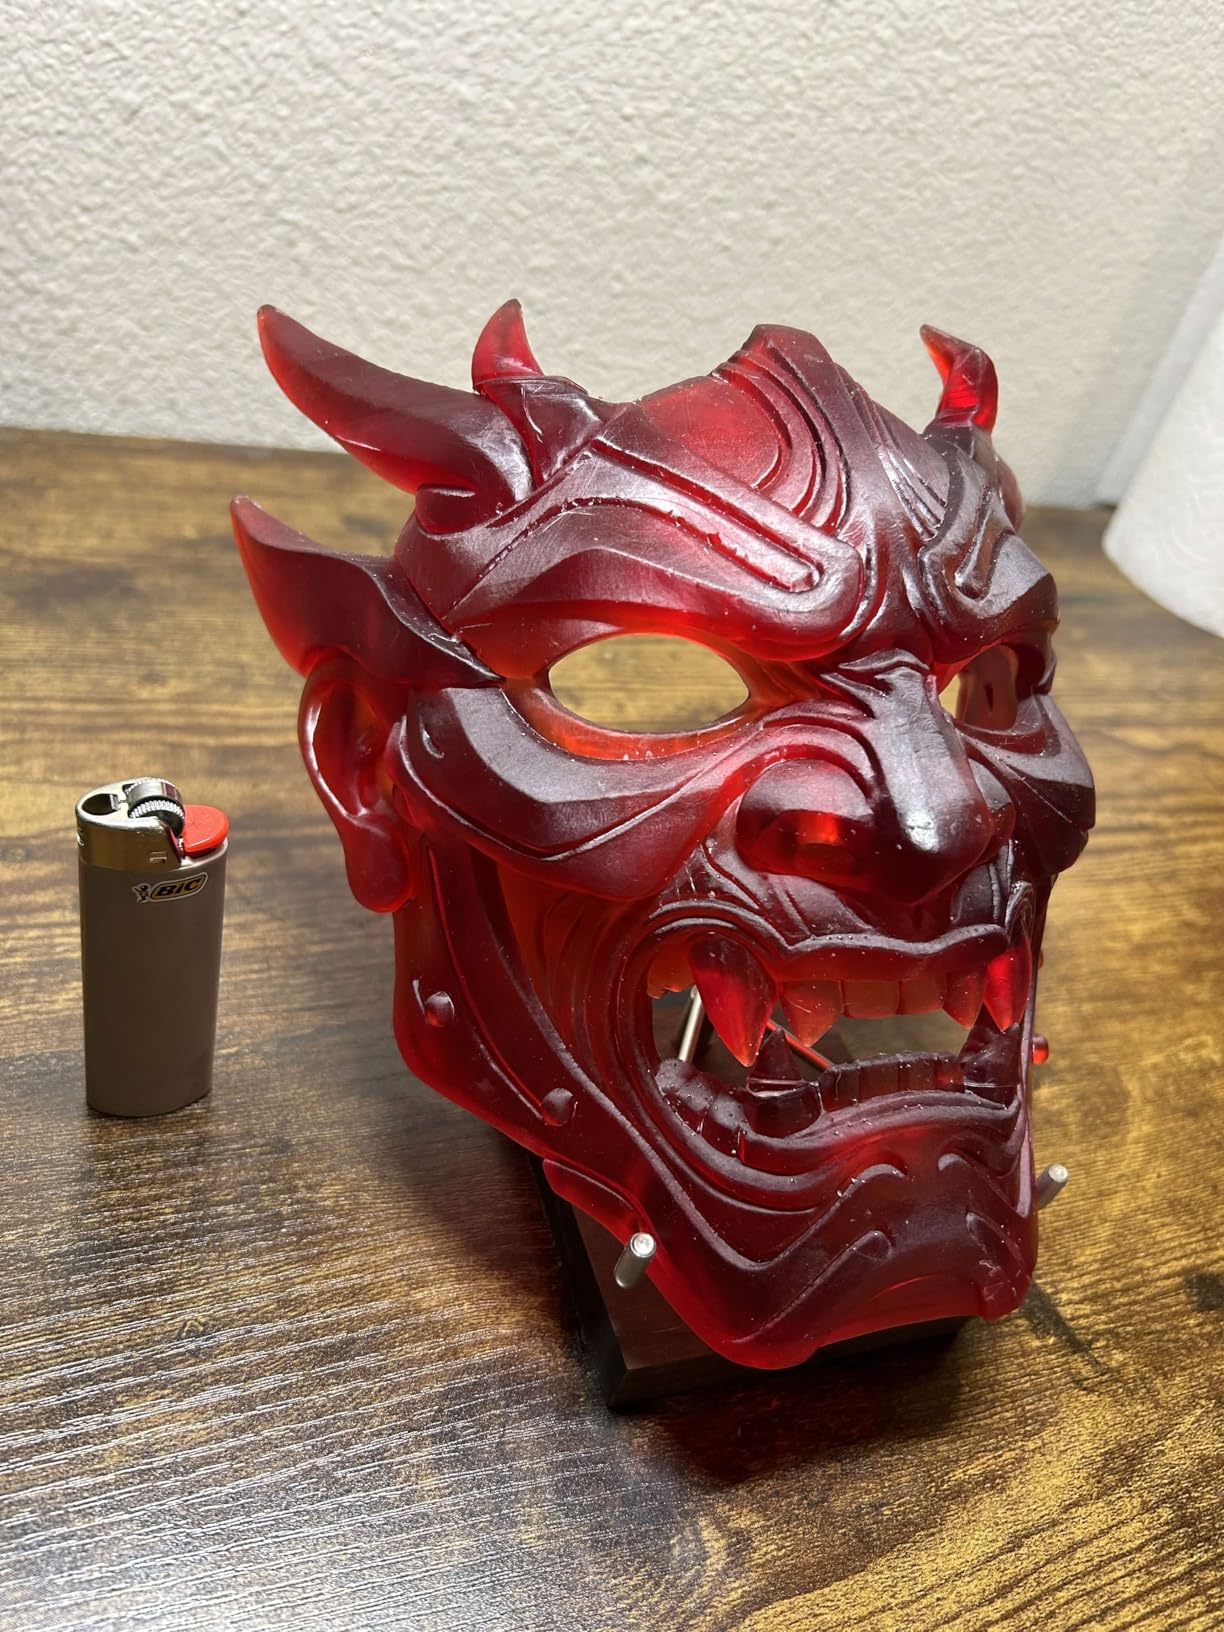
Automation is the theme. Automatic leveling means no manual adjustment on a machine you might be setting up at midnight the night before a deadline, tilt release technology peels a part off the plate fast without the drag that can snap thin features, and the AI camera with chamber lighting gives you monitoring and time-lapse capture of long detail prints.
Where this is the right machine
Small and medium resin parts where finish is everything: visors, lenses, small trim, clasps, weapon details, and anything that will be handled and looked at closely. Print speed up to 150 mm/h with tilt release means a batch of small parts is a short job, which is exactly how you want a detail machine to behave alongside a big FDM machine running armor.
It is also the lightest resin machine here at 35.5 pounds, which makes it the most practical of the resin options if your resin work is occasional and shares a room with a printer you run overnight.
Where you will outgrow it
This has the smallest build envelope of the resin machines in this list. A full-size mask or a large shoulder piece is a split-and-join project on this machine, with the seam work that means. If your resin work is mask-scale rather than accessory-scale, the Mono M7 Max is the direct upgrade.
Resin washing, curing, and safety handling apply here as they do everywhere, and 13 percent one-star suggests some early-unit quality issues worth testing before a big job. The residue detection sensor that protects the LCD screen is a nice touch that reduces the most expensive failure mode on a resin printer.
10. Phrozen Sonic Mega 8K S – Best for High-Volume Resin Batches
phrozen Sonic Mega 8K S LCD/MSLA Resin 3D Printer, 43 µm High Resolution, 15 inch Mono LCD Screen, Fast Production Accurate Details, Large Printing Size L12.99xW7.28xH11.81 Printing Volume
MSLA resin
33 x 18.5 x 30 cm plate
43 micron 8K screen
ACF film
57.3 lb
Pros
- Very large build plate prints many parts per run
- ACF film and TR300 resin for very fast cycles
- Built-in metal drip hanger recovers resin
- Lift-up lid suits a cramped workspace
- Up to 80 miniatures in 90 minutes
Cons
- No WiFi camera or auto-leveling
- Repeated hardware failures reported
- 21 percent one-star is the highest critical share here
- 43 micron is coarser than 12K and 16K panels
The Sonic Mega 8K S is a production machine that happens to be useful for cosplay. A 33 x 18.5 x 30 cm build plate is enormous by resin standards, and the manufacturer quotes up to 80 one-thirty-second scale miniatures in 90 minutes. Even discounting the marketing number for real-world overhead, that is a lot of small parts per cycle, which is exactly the shape of a cosplay accessory batch.
The speed comes from the ACF fluoropolymer film paired with TR300 high-speed resin, which is engineered to release from the film quickly, combined with reduced suction force that improves success rates during continuous production. On a batch job that is the difference between running the machine overnight and running it for four hours.
Two practical details matter more than the spec sheet for cosplay work. The lift-up lid design reduces vertical and lateral clearance requirements, so it works in a cramped room where a flip-open lid would hit a shelf. And the built-in metal drip hanger lets you hang build plates to recover resin, which on a large plate full of parts is a meaningful ongoing saving.
At 43 micron XY resolution on a 15 inch 8K mono LCD, the detail is good rather than exceptional, and it is coarser than the 12K and 16K panels elsewhere in this list. For a batch of buckles, vents, and trim rings that is perfectly fine, because none of those parts are defined by a 0.01 mm edge.
Where it beats the alternatives
Batch economics. If your cosplay project involves a set of repeated parts, a large resin plate gets you more finished pieces per resin bottle than any other machine here, and the fast release cycle means more cycles per night. Enthusiastic owners cite the build volume and speed for large props and batch work as the main reasons they bought it.
Support is worth mentioning too: one reviewer reports a support request resolved quickly when an LCD needed replacement, which is the failure you cannot work around.
The reliability record is the concern
Several buyers report repeated hardware failures including LCD controller boards and power supplies, plus components arriving damaged or cracked. At 21 percent one-star, this is the highest critical share of any resin printer in this roundup, and that is a real risk to weigh against a 49-review sample, because 21 percent of 49 is a small number of units but a meaningful proportion.
There is also no WiFi, no camera, and no auto-leveling. You level it by hand, every time, which is a meaningful quality risk on a large plate where the whole point is unattended batch production. If you can accept manual leveling and want the best finish rather than the most parts, the Saturn 4 Ultra 16K is the better detail machine, and if you want the largest verified resin volume, the Mono M7 Max has far more owner history behind it.
FDM or Resin for Cosplay Props: How to Decide
Use FDM for anything large, hollow, wearable, or heat-exposed. Use resin for anything small, detailed, dimensionally precise, or that needs a finish you are not going to sand for six hours. That is the whole decision, and it has not changed in 2026 despite every machine in this list being new.
The reason is mechanical, not aesthetic. FDM lays down material that can be tuned for toughness: increase wall count, drop infill, and the part gets stronger while getting lighter, which is exactly what a convention-worn chest plate needs. A resin part is strong in compression and brittle in a thin section, so the place it fails is the place it will get knocked.
Resin wins for a different reason: it is a photopolymer, so a cured surface is smooth at a scale FDM cannot reach. A 16K panel on a small prop produces a finish you can prime and paint with minimal work, while the same part in FDM needs sanding through layer lines. If the part is smaller than your hand and will be looked at closely, resin is the faster path to a good result.
Cost per gram runs the other way. FDM filament is measured in grams and a hollow chest plate uses a manageable amount; resin is measured in milliliters and large prints are expensive unless you hollow them and cut drain holes. If a build is resin-heavy in volume, the machine is the cheaper decision and the material is the expensive one.
Safety is the final differentiator and the most commonly underestimated. Resin printing is a ventilated-room activity with gloves, a wash station, IPA, and a UV cure step, and that workflow is what puts a lot of first-time buyers off. The honest answer is that resin is not unsafe if you respect it, but it is a workflow commitment that FDM does not ask you to make.
How Big a 3D Printer Do You Need for Cosplay?
Measure the largest single piece you want to print in one go, and buy a build volume that clears it with a little room. That is the entire sizing rule, and the reason it matters so much is that splitting a part is the single most common regret reported in cosplay printing threads. A seam on a helmet cheek is a sanding and filling job; a seam across a chest plate is a structural and visual problem.
For a specific piece, the math is straightforward. A full-size human head is roughly 230 mm tall with a helmet shell and chin extended. A chest plate for an adult is commonly 300 to 400 mm across and a full adult torso back plate is wider. A shoulder pauldron on a large build can exceed 250 mm on its own. A forearm gauntlet usually fits in 200 mm.
As a general ladder: a 150 mm cube handles gauntlets, buckles, trim, and prop details, and you will split everything above that. A 250 mm cube handles a forearm piece, a boot, or a medium accessory in one go. A 350 mm cube takes a full helmet, a chest plate, and most shoulder pieces without splitting. A 390 mm class machine takes the largest single torso plates and full helmets with clearance to spare.
On r/cosplayprops the consensus is blunt about this: size matters more than almost any other specification, and the advice given repeatedly is to go bigger for large prop pieces and full-size helmets. That is why five of the ten machines here have a 350 mm class or larger envelope.
One caveat before you chase maximum volume. A large build volume is only useful if the machine is rigid enough to hold precision at the edges of that volume and if bed adhesion holds for the whole print. A small well-built machine that prints a 200 mm part cleanly beats a large machine that lifts at the corners on a 12 hour job, which is why mesh leveling, a full heated bed, and a rigid frame belong in the same sentence as volume.
Best Filament and Resin for Cosplay Armor
PLA and PLA Plus for most armor, PETG for anything that gets handled or flexed, ABS or ASA for heat and impact, and tough resin for rigid detail parts. That mapping covers the overwhelming majority of cosplay work, and the machine only needs to support the top two rows of it for a typical build.
PLA and PLA Plus are the default because they sand and paint beautifully, print cleanly without an enclosure, and are the easiest material to tune. Their weakness is heat and impact. A PLA chest plate left in a hot car on the drive to the convention can soften, and a PLA gauntlet that gets knocked on a door frame can snap. If the part will be worn hard, step up.
PETG is the practical upgrade for wearables. It is tougher, more flexible, and far more forgiving of a knocked corner, with a slightly rougher surface that actually primes well. It prints at a similar temperature to PLA with minimal enclosure needs, so it costs you nothing extra in machine capability. The trade is that PETG strings more and needs a bit more tuning on retraction.
ABS and ASA need a heated, ideally enclosed chamber. ASA is the better outdoor choice because it holds up to ultraviolet exposure far better than ABS, which matters for anything that will be in daylight or on a display. Both need a machine with a chamber, which rules out the A1 Combo and is the entire reason the enclosed machines in this list cost what they do.
TPU is for soft goods, straps, grips, and costume-safe edges that touch skin. Nylon and carbon-filled nylon are for functional hard points, buckles, and weapon grips, and they need an all-metal hot end and a hardened nozzle. The P1S explicitly does not recommend fiber-reinforced polymer, which is a real limitation if a build depends on CF material.
On the resin side, standard resin is for display detail where impact is unlikely. Tough resin is for functional parts that will be handled, and it is the resin to reach for on a prop you will carry around all weekend. Flexible resin is for trim, straps, and costume pieces that need to bend against skin. Whatever you use, hollow large resin prints and cut drain holes, because that is the single biggest lever on resin cost.
One settings note that matters more than the material choice for a wearable piece: wall count beats infill for strength. A builder on r/3Dprinting described using four wall loops with low infill on large props specifically to control weight, and the principle generalizes. Most of the strength in a printed part lives in the walls, so put your filament budget there.
How to Print a Prop Bigger Than Your Build Volume
Split the model in your slicer, print the sections flat or in their most stable orientation, then join them with a scarf joint, a lap joint, or a keyed alignment jig. This is the workflow experienced builders use for props that exceed any consumer machine, and it is more reliable than it sounds once you plan the seams.
Choose seam locations deliberately. A seam that crosses a face, a crest, or a panel line is visible; a seam along the underside of a shoulder piece or down the back of a forearm is invisible once assembled and painted. Most slicers offer a simple horizontal cut plane, but the professional move is cutting on a curve and adding a tongue-and-groove profile so the two halves key together and cannot rotate.
Design the joint before you print, not after. A plain butt joint is the weakest option because it relies entirely on adhesive across a flat face. A scarf or lap joint multiplies the glue surface and resists twisting, and a keyed profile stops the halves sliding while the adhesive cures. Add a printed alignment jig if the part has any internal geometry that needs to line up.
Print the sections in the flattest orientation possible and put the seam on the bottom of the print. This minimizes the visible top surface that has to be sanded, and it means the seam is not in the place a camera or an audience looks first. Add a small chamfer on each mating face so the two halves locate themselves instead of requiring perfect pressure.
Join with a rigid epoxy or a solvent-welded ABS/ASA joint for FDM, and mechanical reinforcement for resin. For resin, a scarf joint plus CA glue and a printed alignment guide is the standard approach, and reinforcing the inside with a printed rib is what stops a large hollow shell from cracking along the seam after a con weekend. Test the joint on a small offcut first, because getting the fit right matters more than the print time.
Design for transport while you are at it. A prop that has to travel in a suitcase should be sectioned at the joins anyway, which makes segmentation a packing feature as well as a size feature. That is a real design constraint from convention practice, and a segmented prop that assembles in a hotel room is worth more than a single rigid piece that will not fit in the vehicle.
The hybrid alternative deserves serious consideration. Using foam for bulk sections and printing only the detailed and repeating elements is described on r/cosplayprops and r/3Dprinting as the standard approach for large builds, and it is usually faster, lighter, and cheaper than printing a solid large volume. A printed shell over a foam core gives you the detail where it shows and the low weight where it matters.
Making Printed Armor Light Enough to Wear All Convention Day
Print walls first, infill second, and hollow everything you can. Weight is the number one complaint about printed armor on every cosplay forum, and it is a design and slicing problem before it is a printer problem. A well-sliced chest plate can be light enough for a full convention day on a smaller machine than you would expect.
Start with wall count. Four to six perimeters carry nearly all of the structural load in a printed part, and adding infill past 15 percent adds weight and print time for very little additional strength. A common working setup is four wall loops with 10 to 20 percent gyroid or cubic infill, which is the exact approach one builder described on r/3Dprinting for large props.
Gyroid and cubic infill are worth the slight time premium over rectilinear grid because they pack more strength per gram and they self-support at most angles, which means fewer supports to remove from the inside of a piece you cannot reach anyway.
Layer height is a quality-versus-time dial, and for wearable armor the middle setting is usually right. Coarser layers print faster and are lighter; finer layers look better and hold detail edges more crisply. On a piece that will be sanded and primed anyway, the extra time for very fine layers often buys nothing visible.
Hollow large FDM parts and resin parts alike. On resin, hollowing with drain holes is the standard technique and can cut material cost dramatically on a large piece. On FDM, printing in vase mode or with a low top and bottom solid layer count makes a light shell that is easy to sand, and it also reduces the print time, which helps with the deadline problem as much as the weight problem.
Add reinforcement only where it earns its weight. A chest plate needs reinforcement at the strap anchors and the neck opening, and a gauntlet needs it at the wrist and finger joints. Everywhere else, a hollow shell with good walls is enough, and the grams you save there are the grams you are not carrying for ten hours a day.
Finally, plan the mounting. Foam or EVA padding against the body, straps routed to load-bearing points rather than decorative ones, and a design that lets you get it on and off in under a minute, all matter more for a long day than a small change in infill. A prop you can put on quickly is a prop you will actually wear for the whole convention.
Resin Safety, Washing, Curing and the Post-Processing Chain
Nitrile gloves, ventilation, and a proper wash and cure step are non-negotiable if you print resin. Uncured photopolymer is a sensitizer, and skin contact over repeated sessions is how people end up with a dermatitis problem that ends their printing. The workflow itself is straightforward once it is set up.
Work in a ventilated room, ideally with the printer in a position where fumes are not directed at your face, and wear nitrile gloves for every handling step from removal to finishing. Keep dedicated tools for resin work, because the same bottle that cured on your bench will not go back into a filament setup.
The chain runs in one order: print, remove, wash in IPA, cure under UV, then finish. Washing removes the uncured skin that would otherwise stay tacky forever and block light in the next print, and curing fully before sanding is what makes resin hard enough to sand without gumming the paper. Do not skip the cure step and go straight to filler primer, because uncured resin will still be soft under the primer.
For FDM, the chain is sand, fill, sand, prime, paint. Layer lines on a large flat armor surface are the most visible flaw in the entire process, and filler primer applied thin, sanded back with progressively finer grit, and repeated two or three times will do more for the final look than any printer choice. Judge the part after painting, not after printing, because that is the only surface anyone sees.
Airbrush and clear coat finish the job. A matte or satin clear coat over acrylic base coats locks the paint down against handling, and a satin finish hides layer line texture better than a high gloss, which paradoxically makes imperfections more visible. Our cosplay photography lighting guide covers how finish and lighting interact when it comes time to shoot the finished build.
Plan the post-processing time into your schedule, not after it. A helmet that prints in eight hours can easily take fifteen to twenty hours of sanding, filling, priming, and painting. Experienced builders build that labor into the deadline rather than discovering it, and it is the most common reason a convention-ready costume is late.
How We Picked These Printers
We built this list from published specifications and aggregated owner review data, and we filtered hard on one criterion first: does the build volume actually clear cosplay-scale geometry. Anything that tops out at a small cube was excluded regardless of how good it is otherwise, because it forces a split-and-join workflow on every large piece.
From there we weighted four things. Build volume against the size of the part you want to print. Whether the machine is enclosed, since that determines whether ABS and ASA are available. Multi-material capability, because multi-color printing is a decisive purchase factor that most competing guides ignore entirely. And the volume and consistency of owner reviews, because a machine with 2000 ratings tells you far more about real-world reliability than a specification sheet does.
Where review data showed a meaningful reliability concern, we kept the machine and said so. The Creality K2 Plus, the Phrozen Sonic Mega 8K S, and the IdeaFormer IR3 V2 all carry documented hardware or reliability complaints in their owner feedback, and hiding that would make the list less useful rather than more. We weighted long-term owner history heavily, which is why a machine with a smaller review count can appear with a more cautious verdict.
Cost per finished part, not sticker cost, shaped the ranking. Resin printers that force you to buy 500 ml of resin to make one mask rank lower than resin printers with a large vat, and a machine that can print a part in one piece ranks higher than one that needs the same part in three sections. The most heavily reviewed machine in the set, at more than 2000 ratings, took the top spot.
This is a 2026 list and the hardware generation in this space moves fast. We plan to re-check these machines annually, and we re-test as the model generation turns over rather than carrying forward picks whose successors are already shipping.
Frequently Asked Questions
What is the best 3D printer for cosplay?
For most cosplay builds the best 3D printer is an enclosed FDM machine with a 350 mm class build volume and a multi-material unit. It prints full-size helmets and chest plates in one piece, handles ABS and ASA for heat-exposed props, and multi-color printing removes hours of hand painting. A resin printer is the right complement for small detailed parts rather than the main machine.
What is the best 3D printer for making cosplay armor?
Armor needs a large build volume, a rigid frame, and a heated or enclosed chamber. The Anycubic Kobra S1 Max Combo and the Creality K2 Plus Combo both give you a 350 mm cube with a 65 C or 60 C chamber, while the QIDI Max4 Combo goes to 390 mm for full-size plates in one piece. Print hollow with four or more walls and low infill to control weight.
How big of a 3D printer do I need for cosplay?
Buy a build volume that clears your largest single piece with some room. A full adult helmet is roughly 230 mm tall, a chest plate commonly runs 300 to 400 mm across, and a large pauldron can exceed 250 mm. A 350 mm cube covers most full-size armor without splitting, and anything larger than your build volume must be sectioned and joined.
What is the best 3D filament to use for printing armor?
PLA and PLA Plus for most armor because they sand and paint well. PETG for gauntlets, bracers, and anything that gets knocked or flexed, since it is tougher and more forgiving. ABS or ASA for heat-exposed or outdoor props, which requires an enclosed heated chamber. On TPU for soft goods and costume-safe edges, and put your filament budget into wall count rather than infill.
What 3D printer should I buy in 2026?
An enclosed FDM machine in the 350 mm build volume class with a multi-material unit is the most broadly useful purchase for cosplay in 2026. Our top pick, the Anycubic Photon Mono M7 Max, is the resin complement for masks and detail parts, and the Bambu Lab P1S Combo is the strongest all-round FDM choice with a bundled AMS.
Is there anything illegal to 3D print?
Printing a design yourself for personal use is generally treated differently from reproducing a copyrighted work commercially. The realistic risks are selling prints of protected characters at conventions and using commercially licensed files you do not hold. Buying a file from a reputable marketplace and printing for yourself is common practice, but distributing the file or selling finished copies carries real legal exposure.
Final Verdict on the Best 3D Printers for Cosplay Props
The Anycubic Photon Mono M7 Max is our best 3D printer for cosplay props pick, and the reason is a combination of a 298 x 164 x 300 mm resin build volume that takes a full-size mask in one pour and a review base of more than 2000 owner ratings. It sets the detail standard for masks, faces, and hardware, and it is the machine we would build a helmet on first.
Pair it with an enclosed FDM machine for anything larger. The Bambu Lab P1S Combo is the best value for multi-color armor work, the Anycubic Kobra S1 Max Combo matches it on speed with a 65 C chamber and bundled filament drying, and the QIDI Max4 Combo is the answer when a full-size chest plate or helmet has to come off the bed in one piece.
Two situations change the answer entirely. If your props are long rather than large, the IdeaFormer IR3 V2 prints a seven foot blade in a single piece. If you are just starting and PLA-only work is enough, the Bambu Lab A1 Combo gets you multi-color printing at the lowest entry point, and you can move up once you know which half of the FDM or resin split your build actually needs.
Whatever you buy, size the machine to the largest single piece you want finished in one go, print hollow with more walls and less infill, and build the post-processing time into your deadline. Those three decisions matter more to whether your costume is convention-ready than any specification on this list.